Abrasive Jumbo Roll Factory Operations Explained for Buyers
2026-09-22
Behind every smooth surface lies a material most buyers never think twice about—until it fails. Abrasive jumbo rolls are the quiet workhorses of metal finishing, wood sanding, and surface prep lines worldwide. But sourcing them isn't just about width and grit; it's about understanding how a factory actually turns resin, backing, and grain into consistent, high-performance rolls. SHENZHEN SUN ABRASIVES has spent years refining that process, and in this guide, we break down exactly what happens on the production floor—so you can make smarter buying decisions without the guesswork.
Raw Material Choices That Show Up in Roll Performance
The choice between cast iron, steel alloys, and engineered polymers isn't just a cost decision—it sets the ceiling for what a roll can handle. A softer elastomer cover will grip and release a delicate web without tearing, but it sacrifices dimensional stability under high nip loads. Hardened steel cores resist deflection in high-speed converting lines, yet they transfer more vibration to the sheet and require precise grinding to avoid chatter marks.
Additives and fillers matter just as much as the base material. Carbon black in rubber compounds changes heat dissipation and static buildup, which directly affects winding tension and edge curl. In food-grade applications, switching from nitrile to silicone may solve temperature resistance but forces you to rethink drive torque because the surface friction drops sharply. These are not trivial swaps; they alter the roll's weight, balance, and how it reacts to moisture or solvents.
Inside a Modern Coating Line: What Buyers Rarely See
Walk past the gleaming control panels and the rhythmic hum of conveyors, and you'll find the real story of a coating line written in the details buyers never get to see. It's not in the spec sheet, but in the way a veteran operator runs a gloved finger along a just-coated edge, feeling for a roughness the sensors missed. It's in the split-second decision to tweak the oven's airflow because the humidity shifted outside, even though the automation says everything is fine. These quiet adjustments, born from years of troubleshooting, are what separate a line that runs well on paper from one that delivers consistent quality on a humid Tuesday afternoon.
Then there's the hidden choreography of changeovers—the five minutes of controlled chaos when one color gives way to another. A buyer might see that as downtime, but inside the line, it's a carefully rehearsed ballet of purging, wiping, and recalibrating. Every drop of leftover pigment matters, every second of overlap is weighed against the cost of contamination. The best lines have turned this into an art form, reducing waste to a trickle and making the switch so smooth you'd swear the machine never paused. That kind of efficiency doesn't show up in a quote; it shows up in your per-unit cost six months later.
Perhaps most invisible of all is the relentless attention to what's not supposed to happen. A modern coating line earns its keep in the margins: the early-morning viscosity check before the first panel runs, the weekly tear-down of a spray nozzle that looks perfectly clean, the logbook entry noting a two-degree drift in bath temperature that was corrected before it became a defect. Buyers rarely ask to see these logs, but they should. They're the difference between a supplier who promises consistency and one who has the scars to prove it.
Why Grit Bonding and Curing Temperature Are Make-or-Break
In abrasive manufacturing, the resin that holds each grit particle to the backing only performs when its cure cycle is dialed in. Cure too low and the polymer never reaches full cross-link density, leaving the bond soft and gummy. Grits then tear out after only a few passes, and the tool dulls long before the abrasive is actually worn down. Push the temperature too high and the resin over-cures into a brittle, glassy state that cracks under load, causing entire clusters of grit to snap off at once. This narrow thermal window is why bonding and curing temperature quietly decide whether a disc cuts clean or becomes scrap.
The problem gets trickier because different resin systems need different heat histories. A phenolic bond might tolerate a sharp ramp to 180°C, while an epoxy formulation demands a slow climb with a hold at an intermediate plateau to avoid trapping volatiles. If the surface skins over too fast during ramp-up, solvents and reaction byproducts get sealed inside, creating micro-voids that weaken every grit-to-resin interface. Even a short dwell-time error can shift the bond strength enough that a batch passes a visual check but fails on a grinding test.
Production reality makes this even less forgiving. Oven hot spots, air-flow shadows, part thickness, and even the mass of stacked trays all change the actual temperature at the bond line—not the set point on the controller. A thermocouple reading taken from the oven wall tells you almost nothing about what the back of the abrasive sheet experienced. Shops that track cure with part-level probes and log every cycle can catch a 5-degree drift before it ruins hundreds of discs. Those that don't end up chasing inconsistent grit life and blaming the grain when the real culprit was always the cure.
Tension Control and Its Ripple Effect on Converting
A winding roll rarely fails all at once. It starts with a subtle shift in tension—barely visible at the nip, easy to dismiss—and by the time the material reaches the slitter or die-cutter, that shift has become a wrinkle, a misregistered cut, or a stretched edge. In converting, tension is not just a machine setting; it is the variable that carries every other variable downstream.
The ripple effect shows up in ways that often get blamed on raw material or operator error. A slight over-tension at the unwind can elongate film or nonwoven just enough to throw off adhesive coat weights, while under-tension lets the web wander and build uneven roll density. These are not isolated incidents. They compound: one unstable zone forces the next section to compensate, and the line ends up chasing a moving target all shift.
What makes tension control different from most process parameters is that it touches everything but is rarely measured directly at the point of consequence. Closed-loop systems with load cells or dancer feedback help, but the real benefit comes when operators stop treating tension as a setpoint to hold and start seeing it as a signal about the entire line. The converters who get this right tend to run quieter machines, fewer splice breaks, and rolls that unwind the way they were wound—predictably.
On-Site Quality Gates That Filter Out Weak Rolls
In most roll shops, weak rolls don't announce themselves until they're already in a stand and causing strip defects. On-site quality gates change that by catching problems before the roll ever gets near a mill. These gates are not just paper checklists; they're physical testing points placed right where rolls are stored, ground, or assembled.
A common gate involves a quick ultrasonic scan at the roll neck and body transition. If there's any indication of subsurface cracking or an inclusion cluster, the roll is flagged immediately. Another gate might be a portable hardness traverse across the barrel face. Rolls that show more than a small hardness drop in one zone get pulled aside, even if they look fine to the naked eye.
What makes these gates effective is their simplicity and proximity. Operators don't need to send samples to a lab or wait for a report. They get a pass/fail signal in minutes, and that keeps weak rolls from ever reaching the mill stand. Over time, this reduces premature spalling and unexpected roll changes, which is exactly what maintenance teams want.
How Factory Storage Conditions Quietly Affect Your Order
You inspect samples, approve pre-production pieces, and track every production milestone. Yet the quietest risk sits off to the side: the warehouse where raw materials rest and finished goods wait for loading. A space with poor ventilation can slowly warp wood, soften carton edges, or let thin rust bloom on metal parts before your container ever arrives. Fabrics stored against a damp wall often pick up a musty odor that stays sealed inside poly bags until a customer opens the box weeks later. None of this looks dramatic at first—just a slow, invisible drift away from the item you actually approved.
The layout and climate of storage also shape whether your order arrives as one consistent batch. In a cluttered facility, workers may pull the newest cartons from a mixed stack, leaving older units to keep aging or absorb more humidity. Without a disciplined first-in-first-out system, you can unload a shipment where one box’s color is a half-shade lighter or a hinge feels tighter than the next. Even mild temperature swings near a loading dock can make plastics and adhesives expand or contract enough to alter fit and alignment. The goods might pass a fast visual check, but the subtle drift shows up later in customer returns.
The hardest part is timing. Many storage-related defects don’t reveal themselves until goods are in transit or resting on a retail shelf, long after the factory has shifted its attention to other orders. By then, tracing the cause back to a humid corner or a poorly sealed pallet is nearly impossible. That’s why factories that treat storage as an extension of quality control—running dehumidifiers, keeping stock off bare concrete, and labeling every pallet with a clear arrival date—tend to produce fewer hidden surprises. A few photos of the actual storage area during your next audit can tell you more than any polished sample room.
FAQ
It's a wide-format coated abrasive master roll—often 1.2 to 1.6 meters wide and several hundred meters long—produced on a continuous line. Buyers typically convert these rolls into discs, belts, sheets, or specialty shapes in their own facilities, so the jumbo roll becomes the raw input for their finished goods. It lets you control cutting dimensions and packaging without investing in coating equipment.
The backing (paper, cloth, polyester film, or fibre) sets the flex and tear strength; the abrasive grain (aluminium oxide, zirconia, ceramic, silicon carbide) drives cutting speed and life; and the resin system—usually a phenolic or modified resin for the maker coat and size coat—bonds everything together. You can't judge a roll by grit alone; the backing weight and resin ratio matter just as much.
First the maker coat is applied to the backing, then abrasive grains are deposited—either by gravity for economical products or by electrostatic coating for sharper, more upright grain orientation. A second resin layer, the size coat, locks the grains in place. The line speed, coat weight, and grain feed rate are all tied together, so small shifts in one parameter change the cut rate and finish quality.
Most lines pass the web through multi-zone ovens where temperature and airflow are profiled along the length. Hanging festoon dryers are common because they let both sides dry evenly and allow some resin flow before hardening. The key is holding residence time steady—if one edge cures faster than the centre, you get uneven flexibility and premature grain shedding.
A typical release includes checking coating weight per square meter, grain adhesion, tensile strength, thickness tolerance, and visual defects like streaks or missing mineral. Some factories also do a flex test or a quick cutting trial on a converted sample. Batch records link each roll back to its raw material lot and oven profile, so a problem can be traced even months later.
Yes, but it's usually a conversation about minimum order quantities and development lead time. You might request a lighter cloth backing for conformability, a ceramic blend for stainless steel, or an anti-static treatment for wood sanding. The factory will run a trial batch, send you a sample roll, and only move to full production once your conversion line confirms the performance.
Look at their coating width capability versus your converting needs, whether they use electrostatic grain application for consistent cut, how they document batch-to-batch variation, and whether they can store and ship rolls without crushing the edges. A supplier with a responsive technical team is often worth more than a 2% price difference, because a bad roll can stall your whole finishing line.
The roll should be wound with consistent tension and wrapped with moisture-resistant film or heavy kraft paper. Many factories use edge protectors and suspend the cores to prevent flat spots from sitting on the floor. Labels need to show direction of unwind, grit, backing code, and production date so the warehouse can rotate stock properly.
Conclusion
Abrasive jumbo rolls may look alike on a spec sheet, but what happens before slitting determines how they behave on your converting line. The raw material choice, whether a heavier cotton blend, polyester film, or a specialty paper, sets the baseline for tear resistance, flexibility, and grain adhesion. Inside a modern coating line, buyers rarely see how the maker applies the make coat, controls electrostatic grain projection, and then cures the resin at a precise temperature window. Get the bonding or curing slightly wrong, and the roll can shed grit early or glaze under heat. That is why serious suppliers treat those stages as make-or-break, not just routine steps.
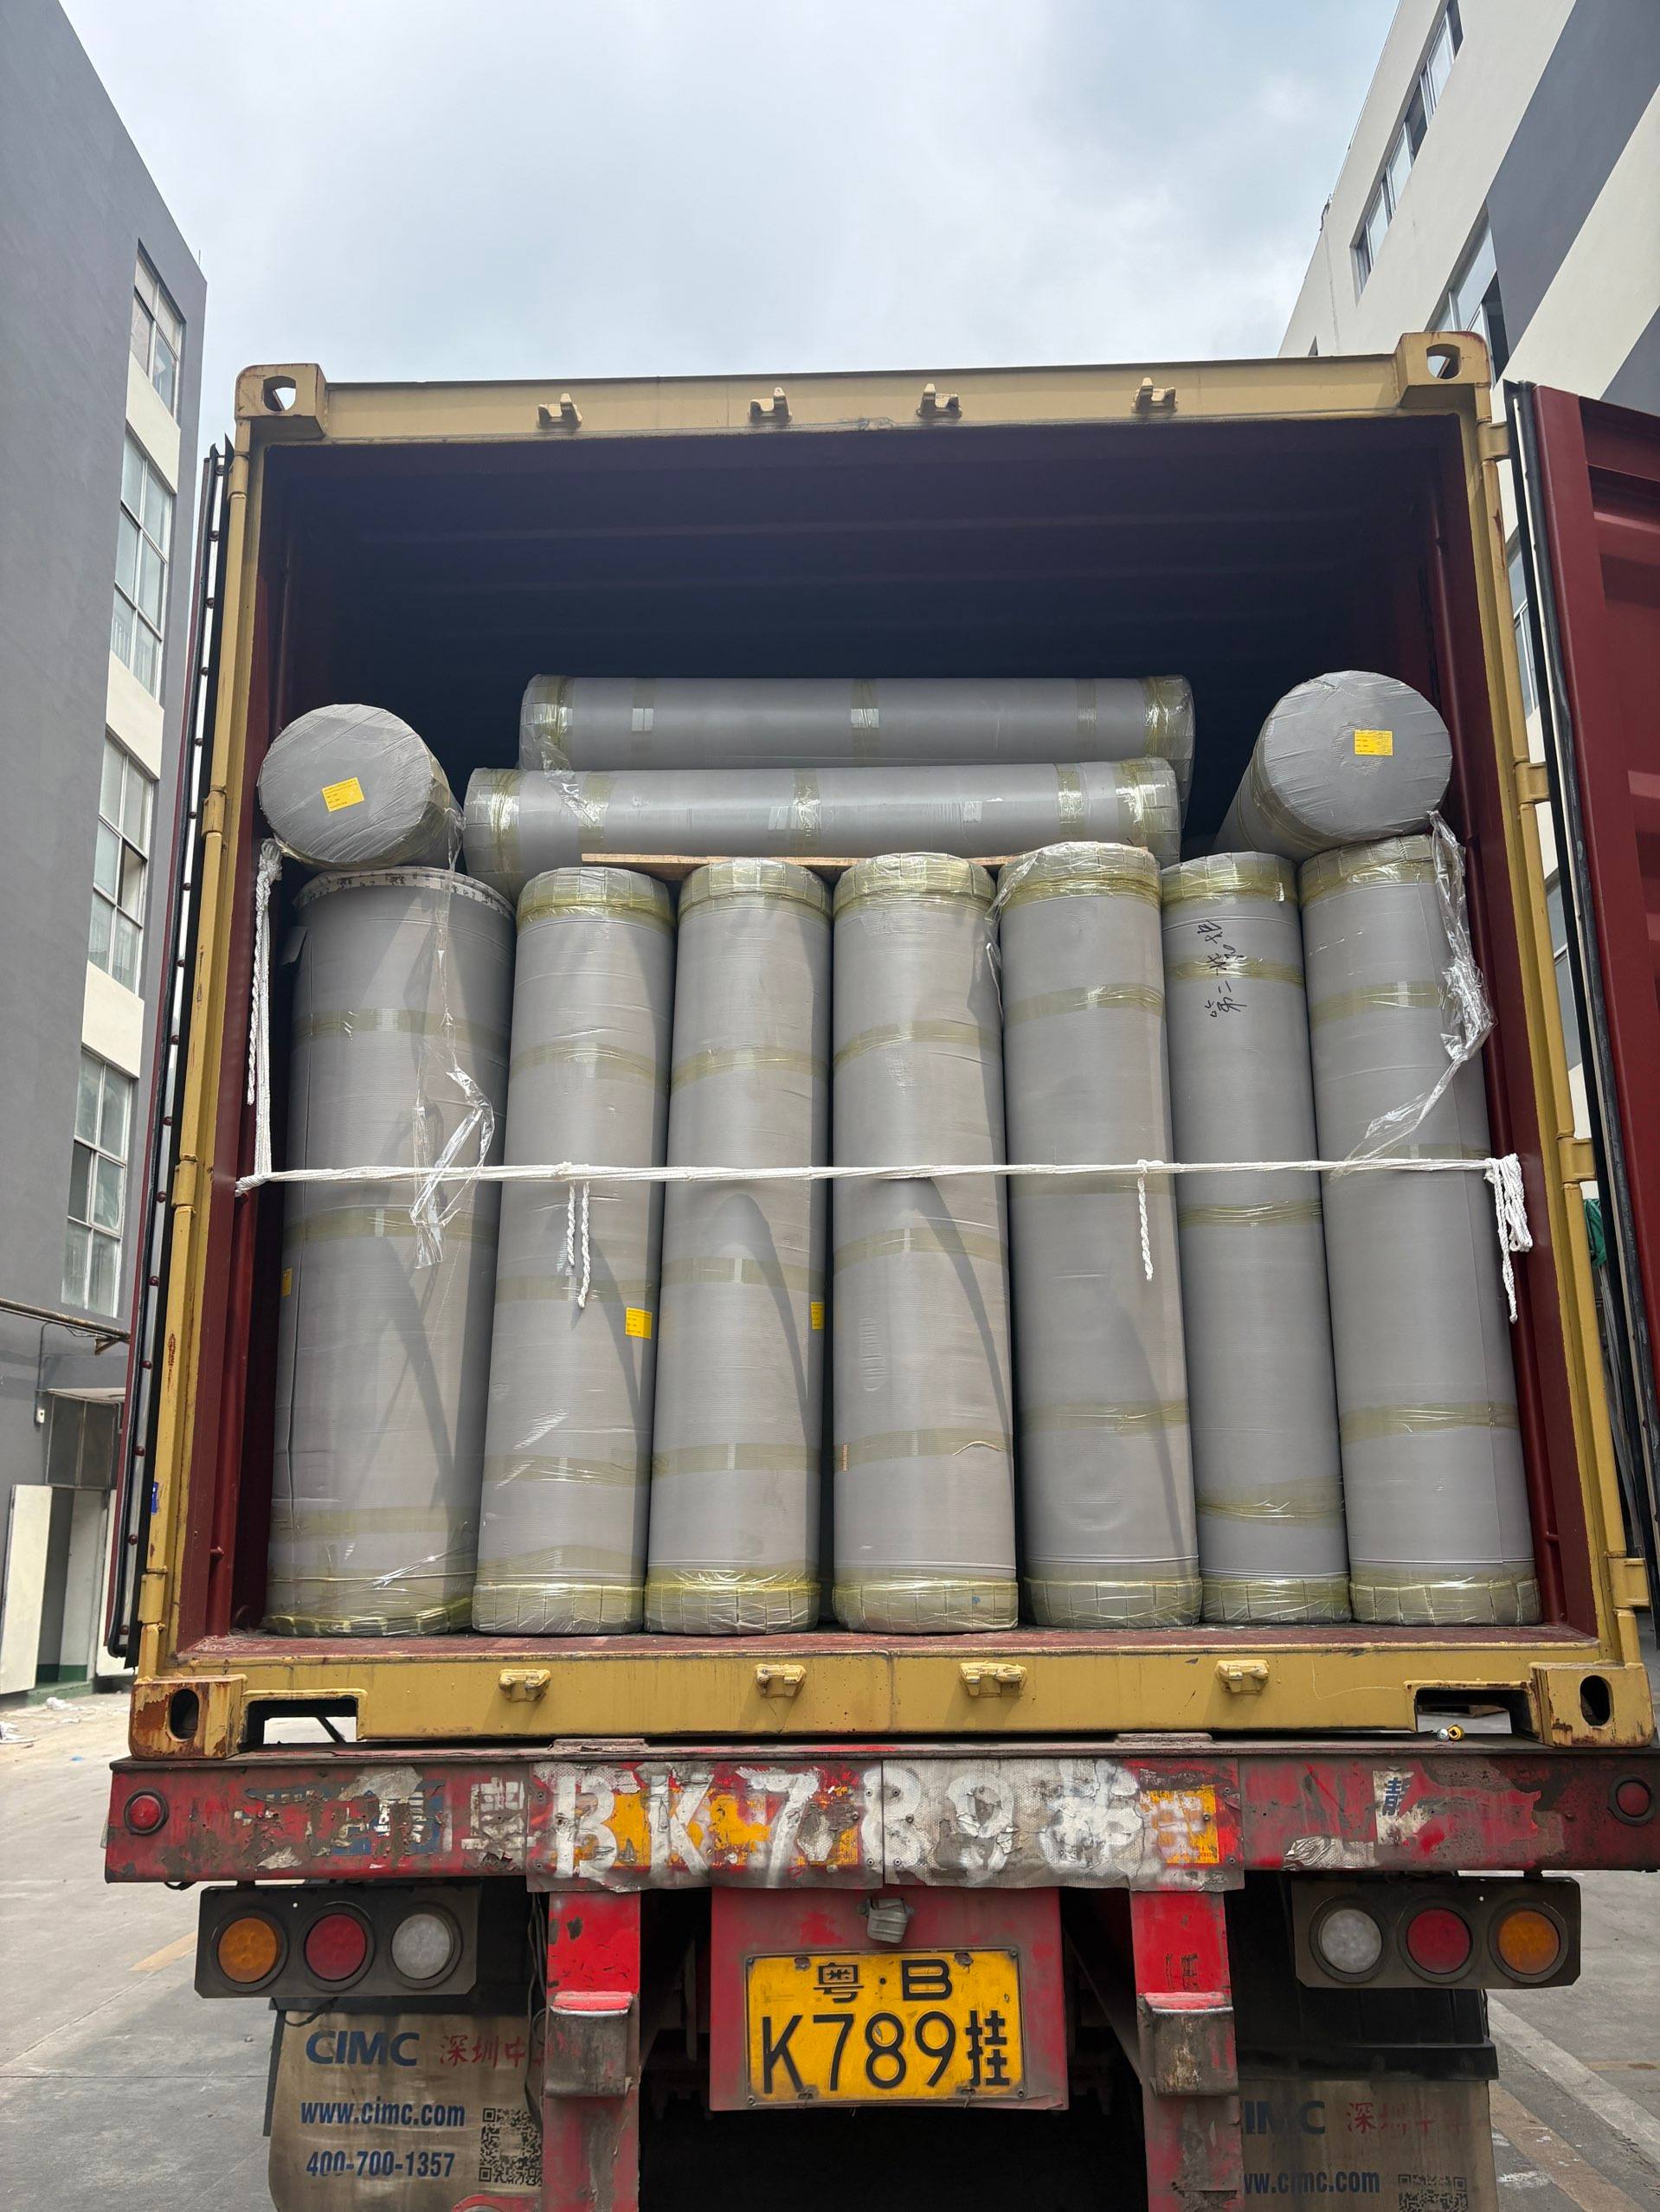
Tension control is another behind-the-scenes factor that ripples into your slitting and die-cutting. A roll wound with inconsistent tension can develop soft spots, telescoping, or edge nicks that show up only after you start converting. On-site quality gates help filter out weak rolls before they ship, but they only work if the factory checks the right things: total weight, unwind profile, and a peel or abrasion test on a sample strip. Storage conditions play a quiet role too; humidity and temperature swings in a warehouse can curl the backing or alter resin cure, especially for rolls sitting near dock doors. Buyers who ask about these details usually get more predictable performance out of every jumbo roll.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn