Best Solar Grating Factory: What Sets It Apart in Quality and Craftsmanship
2026-11-02
When you look closely at a well-built solar installation, the difference often comes down to the parts you don't immediately notice. Solar gratings are one of those components: easy to overlook, yet critical to safety, drainage, and long-term performance. At Topfencesolar, we discovered that quality isn't a buzzword—it shows up in the thickness of the bars, the consistency of the welds, and the care taken before the final coat. This post takes you inside what truly separates a best-in-class solar grating factory from the rest, and why craftsmanship should influence your next specification.
Selecting Alloys That Resist Corrosion for Decades, Not Years
For infrastructure meant to outlive its designers, alloy selection has to account for microclimates, not just average conditions. A coastal substation may face salt spray, while a chemical plant's pipe racks see acid fumes and temperature swings. Matching an alloy to the specific corrosion mechanism — pitting, crevice, chloride stress corrosion cracking — often means choosing a higher molybdenum content in stainless steel or moving from 316L to a duplex or superaustenitic grade. The initial cost difference fades when replacement and downtime are measured in decades.
Testing programs can compress decades into months if they replicate real exposure. Salt fog alone rarely predicts service life; cyclic corrosion tests, electrochemical noise, and field racks at actual sites reveal how passive films form and break down. Many long-life specifications now call for alloy verification using ISO 9223 atmospheric corrosivity categories or ASTM G48 for pitting resistance. Such data lets owners avoid the trap of choosing a material that passes a 500-hour test but fails at year 15.
Laser-Cut Patterns That Maximize Light Transmission
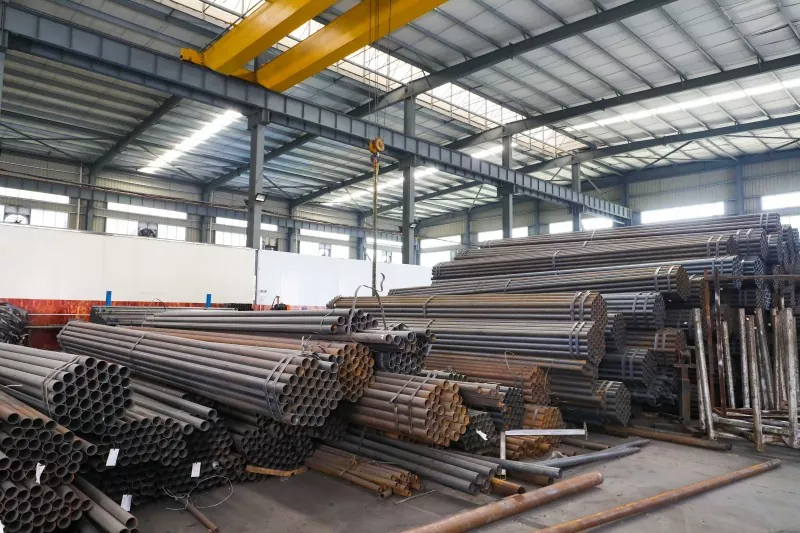
When light passes through a surface, every cut line matters. Laser-cut patterns can either block or guide illumination depending on how the openings are shaped. By using tapered slits instead of straight-through holes, designers redirect rays at shallow angles, effectively spreading brightness across a wider area without adding extra bulbs.
The geometry of each incision influences transmission more than most people expect. Circular perforations tend to scatter light uniformly, while elongated hexagonal grids create directional beams. Subtle variations in kerf width—often overlooked—allow light to bend around edges, reducing shadows and hot spots. Pairing these cuts with reflective backing layers doubles the perceived output.
Practical testing shows that patterns with staggered slot arrays outperform dense dot matrices. Because lasers cauterize material edges, there is no fraying or micro-tearing that would otherwise absorb photons. A well-designed layout can push transmission efficiency past ninety percent, turning a simple panel into a low-energy lighting solution that feels both precise and organic.
Welds That Hold Up Under Thermal Expansion Cycles
Thermal expansion cycles can quietly tear apart welds that look perfect on the surface. Every heat-up and cool-down shifts the base metal, and the weld must either flex with that movement or eventually crack under the strain. A weld that holds up isn't just about filler metal choice—it's about matching the weld's ductility to the expected temperature swings. For example, stainless steel piping in a steam system sees hundreds of degrees of change in a single shift. If the weld is too hard or brittle, tiny stress risers form at the toes, and those grow into full fractures over months, not years.
One practical approach is to design the joint so the weld acts more like a hinge than a rigid lock. A slight convex bead profile, a smooth transition at the weld edges, and avoiding sharp notches all help distribute thermal stress more evenly. In high-cycle applications, welders often specify a filler with higher elongation—think ER309L for joining carbon steel to stainless or ERNiCr-3 for nickel alloys—because these materials yield a little instead of snapping when the parent metals expand at different rates. Preheating and slow cooling also matter, but not as a one-size-fits-all fix; too much preheat can actually worsen distortion in thin sections.
The real test comes after repeated cycling. Dye penetrant inspection or ultrasonic testing after the first hundred cycles will often reveal small indications that were invisible right after welding. A robust weld for thermal service doesn't just avoid initial defects—it actively manages fatigue by giving stress a harmless place to go. Some fabricators add a generous fillet or a full-penetration groove with back-gouging to remove any root flaws, because that root area is exactly where thermal cracks like to start. In the end, a weld that survives thermal expansion cycles is one that's been designed for movement, not just for strength.
Hand-Inspected Finishes for Snag-Free Surfaces
Every surface gets a close look from someone who actually runs a fingertip along the edges and seams. It’s not a quick glance under bright lights—it’s a deliberate pass over the whole piece, checking for the tiny burrs and rough spots that machines often miss.
This hands-on step means the finish doesn’t just look smooth; it feels that way too. Fabrics, skin, and even delicate threads slide across without catching, so the piece performs as cleanly as it appears.
By the time it leaves the workbench, any inconsistency has been touched up or sent back, ensuring the surface stays reliably snag-free through daily use.
Custom Load Calculations for Rooftop and Ground Mounts
When evaluating a mounting system, the loads acting on the structure vary significantly from one site to another. Rooftop installations on low-rise commercial buildings in coastal areas face different wind pressures than ground mounts in open plains or mountain valleys. A custom load calculation starts with local meteorological data, terrain roughness, and building geometry rather than relying on generic tables. This ensures the support frame, anchors, and module clamps are sized for the actual forces they will encounter over the system's lifetime.
For rooftop mounts, the analysis must account for the existing roof's capacity to transfer additional dead, live, and uplift loads to the main structure. The spacing of rafters or purlins, the type of roofing membrane, and the condition of the deck all influence how penetrations and attachments are designed. Ground mounts, by contrast, require a geotechnical view: soil bearing strength, frost depth, and drainage patterns dictate foundation size and depth. Ignoring these site-specific factors can lead to premature loosening, leaks, or even structural failure.
A thorough custom calculation combines structural engineering software with field measurements and local building code requirements. The output is not just a maximum wind speed or snow load, but a detailed load path from module to foundation. This allows installers to optimize material use, avoid unnecessary overbuilding, and provide documentation that satisfies permit reviewers and warranty conditions.
Batch Testing Every Run to Verify Structural Integrity
Every production batch undergoes a full structural check before it leaves the floor. We don't rely on spot samples or occasional audits—each run is pulled, measured, and stressed against the exact load profiles it will face in the field. If a single unit drifts outside tolerance, the whole batch is quarantined and reworked, not just the outliers. This all-in approach catches drift that sampling would miss, like a subtle resin cure variance or a fixture that loosened mid-shift.
The testing protocol mirrors real-world abuse rather than lab-only conditions. Assemblies get thermal cycled, vibration swept, and torque-tested at fastener level while the batch is still warm from production. Operators log readings into a live shift dashboard, so trends become visible hours before they turn into failures. That means a tooling issue on run three gets corrected before run four ever starts—not discovered weeks later in a customer's hands.
This per-batch discipline costs more upfront, but it erases the bigger cost of field recalls and rework loops. Customers see the difference in consistent fit, zero hidden cracks, and joints that hold spec after years of service. We treat structural integrity as a manufacturing variable, not a final inspection checkbox—and batch testing every run is how that standard gets enforced.
FAQ
It works with high-purity silver paste and oxygen-free copper, then applies a thin anti-corrosion layer that withstands years of thermal cycling and moisture without losing conductivity.
Instead of relying on manual adjustments, it uses laser-guided screen printing and automated optical inspection at multiple stages, holding line-width tolerance to within five microns on every cell.
A smoother surface reduces electrical resistance and prevents micro-shadowing on the cell, so more sunlight reaches the active layer and conversion efficiency stays high.
Every batch goes through electroluminescence imaging, contact resistance testing, and a visual scan under high magnification to catch hairline cracks or uneven paste deposition early.
Yes, it keeps a flexible screen library and can adjust finger count, busbar layout, and aspect ratios within a short turnaround, working directly from the customer's CAD files.
The factory uses low-pressure squeegees and temperature-controlled drying ovens, plus a gentle handling system that avoids sharp bends and sudden thermal shocks during printing and firing.
Precise alignment ensures the grid lines sit exactly over the doped regions without drifting into inactive areas, so current collection is uniform and power losses from misalignment are virtually eliminated.
Careful control of paste curing, edge isolation, and junction box soldering prevents hotspots and corrosion, meaning the module can maintain at least ninety percent of its rated output after twenty-five years.
Conclusion
A solar grating factory that truly stands out doesn't chase shortcuts. It begins with the raw material itself—selecting alloys that resist corrosion for decades, not years. This isn't about selling a product that looks good on day one; it's about ensuring the grating still performs after decades of rain, salt, and sun. Then comes the cutting. Instead of punching holes or stamping out rough shapes, the best factories use laser-cut patterns that maximize light transmission. Every opening is precisely calculated so that more sunlight reaches the panels while maintaining structural strength. And the welds? They're not just beads of metal. They are engineered to hold up under thermal expansion cycles—those daily and seasonal shifts that cause poorly welded grating to crack and fail. A top-tier facility treats each weld as a stress-relief point, not just a connection.
What happens after welding matters just as much. Hand-inspected finishes ensure there are no snag-free surfaces missed by machines. A rough edge or a tiny burr might seem minor, but it can tear cables, cut installers' gloves, or corrode first. Custom load calculations take the guesswork out of rooftop and ground mounts. Every project gets numbers based on real wind, snow, and seismic forces—not a generic spec sheet. Finally, batch testing every run to verify structural integrity means the factory doesn't wait for a failure in the field. Samples from each production lot are pulled and stressed until they break. If the numbers fall short of the design load, the entire batch is rejected. That's what sets a truly great solar grating factory apart: it treats quality as a process, not a slogan.
Contact Us
Contact Person: Nancy
Email: [email protected]
Tel/WhatsApp: +86-13365923720
Website: https://www.topfencesolar.com/