Folding Carton Cutting Die Making Equipment Factory Precision Manufacturing Explained
2026-09-01
Precision in folding carton production isn’t a slogan—it’s a daily fight against micro-deviations that ruin crease lines and chew up run speeds. At ADEWO’s cutting die making equipment factory, that fight starts long before steel meets board. Here’s a closer look at the manufacturing discipline behind the dies that packaging plants rely on, and why ADEWO has become a name worth watching in this niche.
The Unseen Step: Stress Relieving Die Boards Before Cutting
Most of the conversation around die board cutting centers on laser power, lens focus, and cutting speed. What rarely gets mentioned is the board itself. Plywood used for die boards carries internal tension from the laminating process, and if you cut right away, that tension can release unevenly as slots are formed. The result is a board that bows or twists slightly, making later steps—like inserting rule or fitting the board into a chase—far more frustrating than they need to be.
A simple habit changes this: let freshly delivered die boards rest flat in your shop for a day or two before cutting. Stack them with small spacers for airflow and keep them away from direct sunlight or damp floors. Some shops add a light, evenly distributed weight on top of the stack to encourage flatness. This quiet step takes no special equipment, but it consistently reduces kerf drift, improves slot accuracy, and means fewer boards get scrapped after the laser has already done its work.
Tight Corners, Sharp Creases: Machining Carton Die Channels
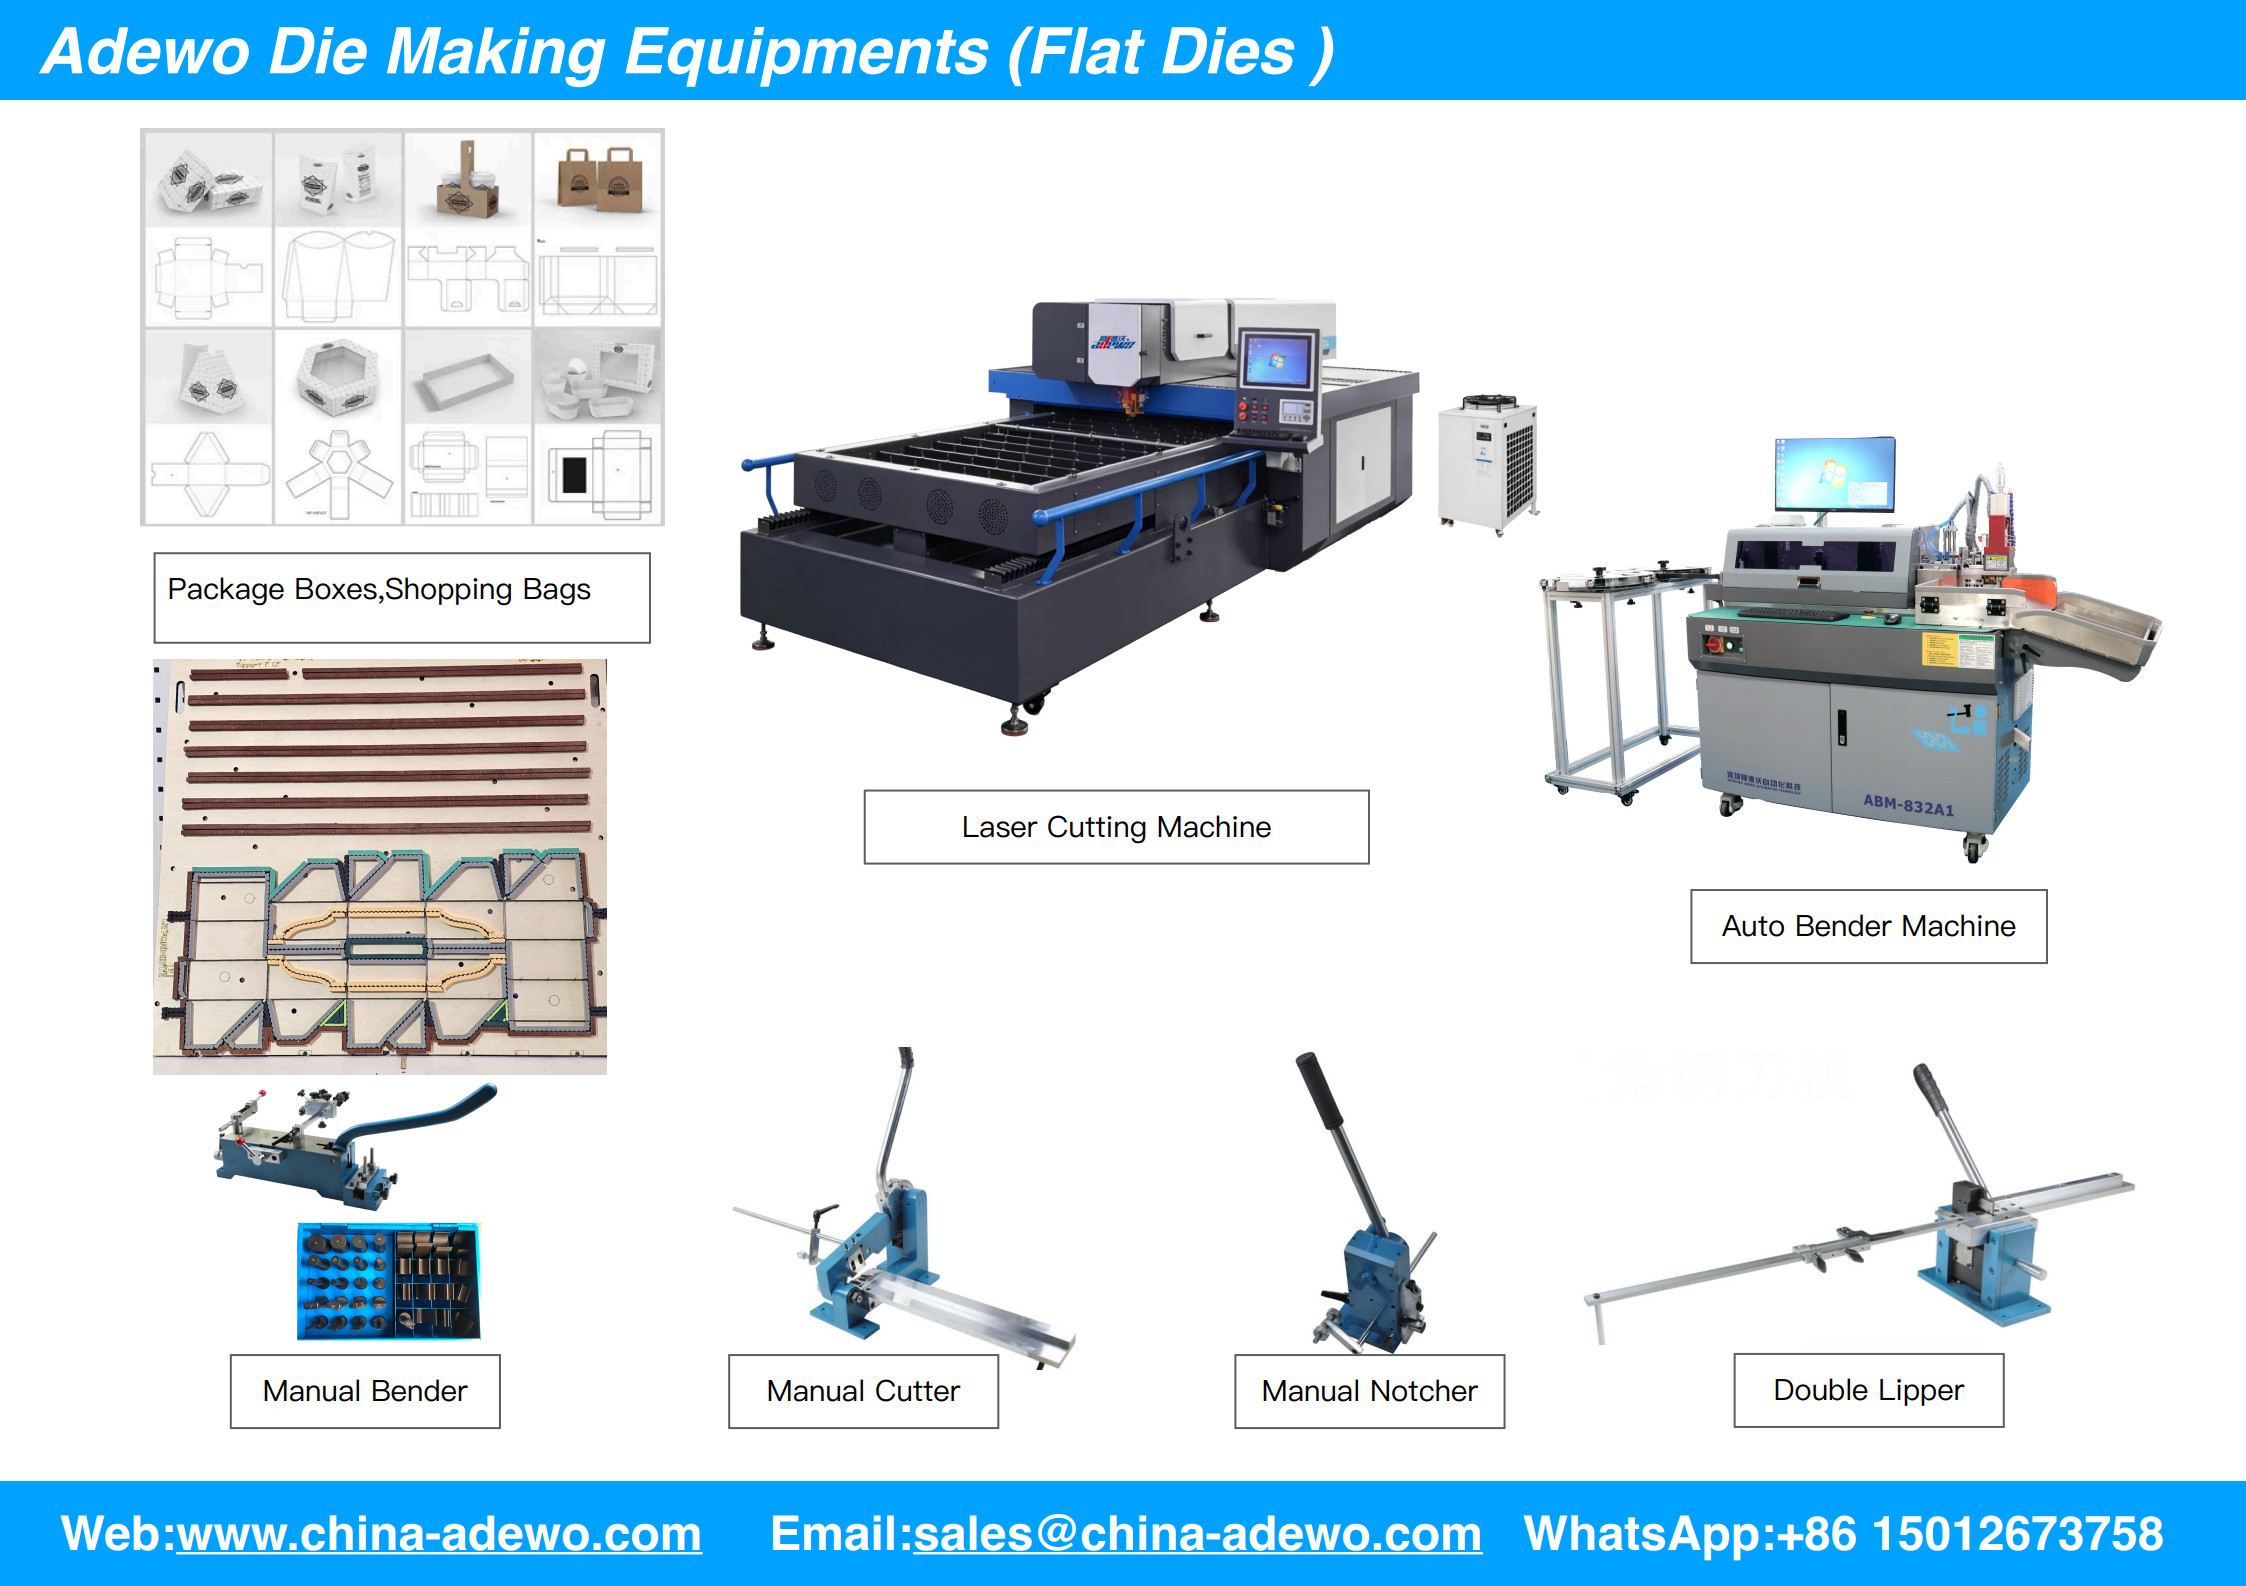
Machining carton die channels is rarely a straightforward milling job. The tight corners demand a cutter path that respects the actual tool radius, otherwise the sharp intersection becomes an unwanted fillet. Many shops try to force a small end mill into the apex and end up with deflection, chatter, or broken tips. A more reliable route is to rough the channel slightly wide, then use a corner-picking pass with a reduced radial engagement to approach the true sharp crease. This staged method keeps the cutting forces predictable and leaves enough material for a final clean-up without overloading the tool at the corner.
The sharp creases along the die channel present a different problem. They act as stress risers during machining, especially if the tool makes a sudden direction change at full feed. Reducing feed rate exactly at the turn—rather than relying on machine look-ahead alone—helps prevent the cutter from pulling into the wall. Some machinists program a slight loop or arc instead of a hard 90-degree stop, but that can round the feature if not tuned carefully. The better compromise is a short linear lead-out past the corner, then a reposition, so the crease stays geometrically crisp while the tool load remains steady.
Material choice also influences how those corners and creases behave after machining. Tool steels used for die plates often release internal stress once the channel is cut, causing the narrow web between adjacent corners to move slightly. To hold the tight geometry, it helps to run a semi-finish pass, let the plate rest, then probe the critical intersections before taking the final 0.05 mm. This way, any drift from thermal or residual stress is corrected in the last pass rather than chasing it with hand filing. The result is a die channel that matches the CAD model at every fold line, without sacrificing tool life or cycle time.
How Cutting Rule Height Gets Checked to the Micron
In a die-cutting shop, checking rule height to the micron isn't a casual glance with a caliper. Most operators start by laying the rule on a surface plate and running a digital drop indicator along its length. The indicator's spherical tip follows the top edge, and any deviation beyond a couple of microns shows up immediately on the readout. But temperature matters—steel expands enough that a hand-held measurement can drift if the part has been sitting under warm lights. So the plate and rule are usually left to stabilize before anyone trusts the numbers.
For tighter tolerances, laser micrometers have replaced contact methods in many plants. The rule passes through a measurement window, and the beam scans its height profile without touching the edge. This avoids the tiny deflection that a stylus can introduce, especially on thin or tall rules. The data feeds into a histogram on the machine's screen, letting the operator see not just a single number but the spread across the whole length. Some shops use this to sort rules into batches that match within a micron or two, which keeps the final cut consistent across a full sheet.
When a Laser Cutter Beats a Router for Die Making
When a die layout moves beyond simple rectangles and straight channels, a router quickly hits its limits. The bit radius dictates the smallest inside corner, and anything tighter forces extra handwork—filing, sanding, or scrapping the board altogether. A laser cutter has no physical radius to fight. It traces the vector path directly, leaving crisp corners and fine slots that would snap a 1/8-inch bit. For steel rule dies and kiss-cut plates, that precision often eliminates an entire finishing step.
Fragile or dimensionally unstable materials also tilt the decision. A router bit pushes down and sideways, which can tear thin plywood, crush flutes in corrugated board, or shift stacked sheets enough to ruin registration. Because a laser cuts without contact, there is no tool pressure to lift or distort the workpiece. This matters most with creasing matrix board, adhesive-backed rubber, and thin acrylic stripping plates, where even a fraction of a millimeter of movement shows up in the final die.
Then there is the speed factor on complex layouts. A router spindle has to physically decelerate, change direction, and ramp up again at every corner, while a laser’s galvanometer or gantry can move from one feature to the next with almost no dwell. Bit wear and chip evacuation are non-issues, and switching materials rarely means re-zeroing or changing a tool. For short-run and prototype die work, the laser often gets a finished board off the machine while the router is still halfway through the second toolpath.
The Wear Patterns That Tell You a Die Needs Resurfacing
Look closely at the die face after a production run, and you will start to see a story in the metal. Fine radial scratches that run from the center toward the edges often show up first. These are not just cosmetic. When they deepen into a crosshatch or start to catch a fingernail, the surface roughness has already passed the point where it can hold a consistent lubricant film. Punches begin to drag, ejection forces climb, and the same scratch pattern repeats on every stamped part until the die is dressed.
Another tell is uneven shine. A healthy die wears evenly, leaving a uniform satin finish across the working face. Once you notice bright, polished islands surrounded by dull, matte zones, the surface is no longer flat. High spots are taking more than their share of contact pressure. Those bright areas will eventually spall or micro-weld to the workpiece, causing sudden galling. If you catch that patchy gloss early, resurfacing removes only a few microns and brings the die back into full contact.
Edge condition matters just as much as the face. Run a bright light along the die radius and look for pitting, fine cracks, or a rolled-over lip. These appear most often at trim edges and deep-draw radii. A small chip might hold for another thousand hits, but it concentrates stress and sends a clear signal that the heat treatment near the surface has begun to break down. Resurfacing before that chip becomes a crack saves the die body and keeps the part profile within tolerance.
Matching Die Steel Hardness to Carton Board Density
The link between die steel hardness and carton board density is rarely discussed but has a huge impact on both blade life and cut quality. Lighter boards like single-wall corrugated or thin folding cartons don't need extremely hard steel. If you use a blade that's too hard on these low-density materials, you often see premature chipping along the cutting edge because the board doesn't offer enough resistance to justify such brittleness. Softer steel in the 45-50 HRC range tends to flex just enough and keeps the edge intact through long runs.
When you move to denser boards—recycled fiber boards, heavy-duty chipboard, or laminated cartons with densities above 0.7 g/cm³—the story flips. These materials put real pressure on the cutting edge, and softer steel will dull quickly or roll over. Here, a hardness of 55-60 HRC works well, and for extremely dense or abrasive boards, powder metallurgy steels pushing past 60 HRC are worth considering. The extra hardness maintains a crisp edge longer, which directly reduces fuzzy cuts and fiber pull-out.
Hardness alone isn't the whole answer. Coatings like titanium nitride can boost wear resistance without making the base steel more brittle, which is especially useful when cutting high-density boards that cause micro-chipping. The real trick is to run a few test cuts on your specific board and adjust not just steel hardness but also bevel angle and creasing rule depth. A bit of experimentation at the start saves a lot of blade changes later.
FAQ
You will usually see a mix of laser cutters, CNC rotary routers, rule processors, and hydraulic die presses. Laser cutters handle the precise cutting of die boards, while rule processors bend and cut steel rule to match the layout. The die press then tests the finished die under production-like conditions before it ships.
Tight tolerances reduce uneven wear on the cutting edges and creasing rules. When the die board slots are cut accurately, the steel rules seat firmly without extra adhesive or shimming. That stability means the die holds its shape longer, so it can survive more impressions before losing sharpness or alignment.
CNC machining automates the cutting of die boards with repeatable accuracy. Instead of relying on manual jigsaws, factories use programmed toolpaths to cut slots and knockouts. This cuts down human error and allows multiple identical dies to be produced quickly, which is essential for long carton runs.
The die board is usually high-grade birch plywood because it stays flat and resists splitting. The cutting rules are made from hardened steel, often with different edge profiles depending on whether they cut paperboard or corrugated stock. Ejection rubber and creasing matrix strips complete the assembly.
Laser cutting produces very narrow kerfs with clean edges, which helps hold thin steel rules tightly. It also makes complex layouts easier to produce without the vibration and blade wander you get from traditional sawing. That precision directly improves register and reduces make-ready time on the press.
Most factories use a combination of optical comparators, coordinate measuring machines, and test cuts on sample board. The die is placed on a flat inspection table, and key dimensions are checked against the CAD file. Any deviation beyond a few thousandths of an inch typically triggers rework before the die is approved.
Regular cleaning of rule grooves and ejection rubber prevents buildup that can throw off cutting depth. Lubricating moving parts on rule processors and checking laser optics for debris also matter. Many shops keep a log of die usage and inspect the board for warping or loose rules after every job.
Conclusion
Trimming die boards for folding carton production rarely starts with the cutting itself. The boards are first put through a controlled stress-relief cycle—often a slow, low-temperature bake—so that internal tensions from lamination and drying don't warp the final layout once channels are routed. Corner work then demands a different level of care: tight radii and crisp crease lines are machined with dedicated micro-tooling, not just a generic end mill. Where the geometry gets too intricate for a router bit to hold tolerance, a laser cutter takes over, vaporizing material without side-loading the plywood and leaving cleaner shoulders for rule insertion.
Once the channels are cut, checking cutting rule height is done under a digital comparator that reads to a micron, flagging any rule standing proud or shy of the reference plane before the die ever touches a press. Over time, wear shows up predictably—rounded edges on high-cycle crease rules, polish marks on the steel face, or a change in the burr pattern along the cutting edge. Those signals trigger resurfacing rather than a full rebuild. Die steel hardness gets chosen by the carton stock itself: denser, clay-coated boards push hardness up to HRC 54–56, while lighter recycled grades run softer, around HRC 48–50, keeping the cutting edge tough without chipping on abrasive fillers.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com