Foot Massager Manufacturer Questions to Ask Before Choosing a Long-Term Partner
2026-11-21
Choosing a foot massager manufacturer for the long haul isn’t a box-ticking exercise. Ask the wrong questions early on, and you’ll be stuck with inconsistent quality, missed deadlines, or a partner who disappears after the first order. That’s why the right questions matter before you sign anything. At XINGBU, we’ve seen firsthand how a little upfront scrutiny separates reliable long-term partners from costly short-term mistakes. So, what should you really be asking? Let’s break down the questions that expose the truth behind the brochure.
What Actually Happens When a Shipment Goes Wrong?
A shipment rarely fails with a single dramatic event. More often it starts as a missed scan, a trailer left sealed over a weekend, or a pallet set aside because one label tore off. The tracking page keeps showing an in-transit status while the freight actually sits in a corner of a cross-dock, waiting for someone to notice. That gap between what the system says and what is physically happening can stretch for days, and it is usually the shipper or consignee who spots the silence before the carrier does.
Once an exception is confirmed, the real work begins behind the scenes. Freight forwarders and brokers start pulling records from warehouse check-ins, driver logs, and customs entries to pin down where the chain broke. In many cases the delay is not caused by a missing truck but by a paperwork mismatch or a damaged barcode that forced the box off the main sort line. The people involved rarely see the whole picture at once, so emails bounce between three time zones while the shipment sits in limbo.
What happens next depends on how the disruption is classified. A short delay might be absorbed by adjusting the next leg or shifting a delivery window. Damage requires photographic evidence, inspection reports, and a claim that can take weeks to resolve. The hardest part is rarely the physical movement; it is reconstructing accountability from fragmented scans and partial updates, then deciding whether to rebook, refund, or repair the relationship with the customer.
Can They Keep the Same Hands on Your Project After Year One?
Agencies often promise continuity, but the real test comes after the first twelve months. The team that wins your business is rarely the same one that shows up for the second year. Key developers get reassigned, account managers move on, and suddenly you're explaining your product roadmap to a room full of strangers. Before signing, ask for specifics: which individuals are actually allocated to the retainer, and what happens when someone leaves? A reliable partner will have a documented transition process that doesn't leave you starting from zero.
Look beyond the polished kickoff meeting. Request a sample of the actual staffing plan for months thirteen through twenty-four. If the agency hesitates or speaks only in vague terms about 'dedicated resources,' treat that as a warning sign. The best shops retain senior people on long-term accounts precisely because they understand the cost of re-onboarding. They can name the developers who would still be on your project and explain how knowledge gets handed over without drama.
Continuity isn't just about the same names on timesheets; it's about institutional memory. You need people who remember why a certain API was built that way, which client requests were rejected and why, and where the fragile parts of the code live. That kind of depth cannot be replaced by documentation alone. Ask the hard question up front: after year one, will I recognize the team on the next call? If the answer is anything less than a confident yes with names attached, keep looking.
How Do They Prove Quality Beyond a Sample Run?
A polished sample only proves they can get lucky once. The manufacturers worth keeping dig into the numbers behind the line: process capability studies, control charts for critical dimensions, and raw material certs tied to each incoming lot. If a tolerance drifts by a few microns between batches, they want to catch that before it becomes your problem.
Beyond the first article, look for evidence of ongoing inspection at the point of production, not just at the end of the line. That might mean automated optical checks on every unit, pull tests at set intervals, or traceability codes that link a finished part back to the exact material coil and machine operator. When something does fail, the record should tell you why quickly instead of triggering a vague 'rework' label.
The strongest signal is follow-through after shipment. A supplier that tracks field returns, shares corrective action reports without being chased, and adjusts its own internal limits based on real-world wear has moved past sample-quality theater. Ask for a quarterly defect summary and see whether it reads like honest math or a marketing slide.
Who Makes the Call When Custom Tooling Needs Changes?
The short answer: it depends on where the change request lands, but rarely does one person own the entire decision. On most projects, the machinist or toolmaker closest to the physical work spots the friction first, and their read on the problem usually carries the most weight. They know which tolerances are already hanging by a thread, which coolant flow patterns cause chip buildup, and which inserts are wearing faster than the print suggests. When they say a pocket needs to shift by three thousandths or a clamping face is flexing under load, engineering tends to listen, because the alternative is spending another week proving the same point with a dial indicator and a pile of scrapped parts.
Once the problem has a name, the actual approval path gets less linear than an org chart would suggest. A design engineer might redline the tool drawing, but the production manager often has to sign off because any change ripples into scheduling, setup time, and fixture inventory. Purchasing gets pulled in when the revision means a different grade of carbide or a coating that the current vendor doesn’t stock. And if the tool belongs to a customer-owned asset, the customer’s own process engineer may have final say, especially in aerospace or medical work where a change without documented validation is a nonstarter. The result is a negotiation, not a handoff.
What tends to separate shops that handle this well from ones that stall is whether the decision-maker on the floor has real authority to test a fix on a single run, document what happened, and bring data back to the table. Some places treat that as a firing offense. Others treat it as how tooling actually improves. The best-run operations make the call as close to the spindle as possible, while keeping a paper trail that satisfies everyone whose name appears on the revision block.
Will Their Capacity Grow Before Your Demand Does?
Scaling looks great on a pitch deck, but actual delivery timelines often tell a quieter, messier story. You need to pin down whether the supplier's expansion plans are tied to real capital, confirmed equipment orders, and hiring commitments—or just optimistic forecasts shared in a sales meeting. Ask for recent examples where they doubled output for another client. If they hesitate, dig into the gap between what they promise and what their current floor space, shift patterns, and warehousing can actually absorb without breaking.
Another angle worth pressing: what happens when your order volume spikes mid-contract? A partner that can reroute production across multiple facilities or flex with third-party logistics gives you room to move. Watch for signs of strain in their existing client base too. If they are already running near full utilization, your "urgent" order might quietly slip to the back of the queue while they service bigger accounts first.
Finally, compare their growth trajectory against your own ramp-up schedule. A supplier adding 30% capacity next year sounds reassuring until you realize your demand could jump 80% in the same period. Ask for a written capacity roadmap with milestones and trigger points for review. That way you are not relying on polite assumptions when the real pressure arrives.
Do Their Lead Times Hold Up During Peak Season?
Mostly yes, but not without some stretching. During last year's Q4 rush, standard production times moved from around 18 days to 26 days on regular items. That is manageable if you plan for it, but it catches a lot of buyers off guard when they assume the spring timetable still applies.
The bigger swings show up on customized or low-volume pieces. One order for 120 walnut console tables slid nine days past the original ship date because their hardware supplier fell behind, not because the workshop was overloaded. If your SKU depends on outside components, expect the quoted lead time to flex more than the base catalog items.
For holiday retail or end-of-year projects, early November is already too late. We now add a 10 to 14 day buffer from October through December and check in weekly once the order is in production. The communication is better than most, but the dates are not locked until the goods actually leave the dock.
FAQ
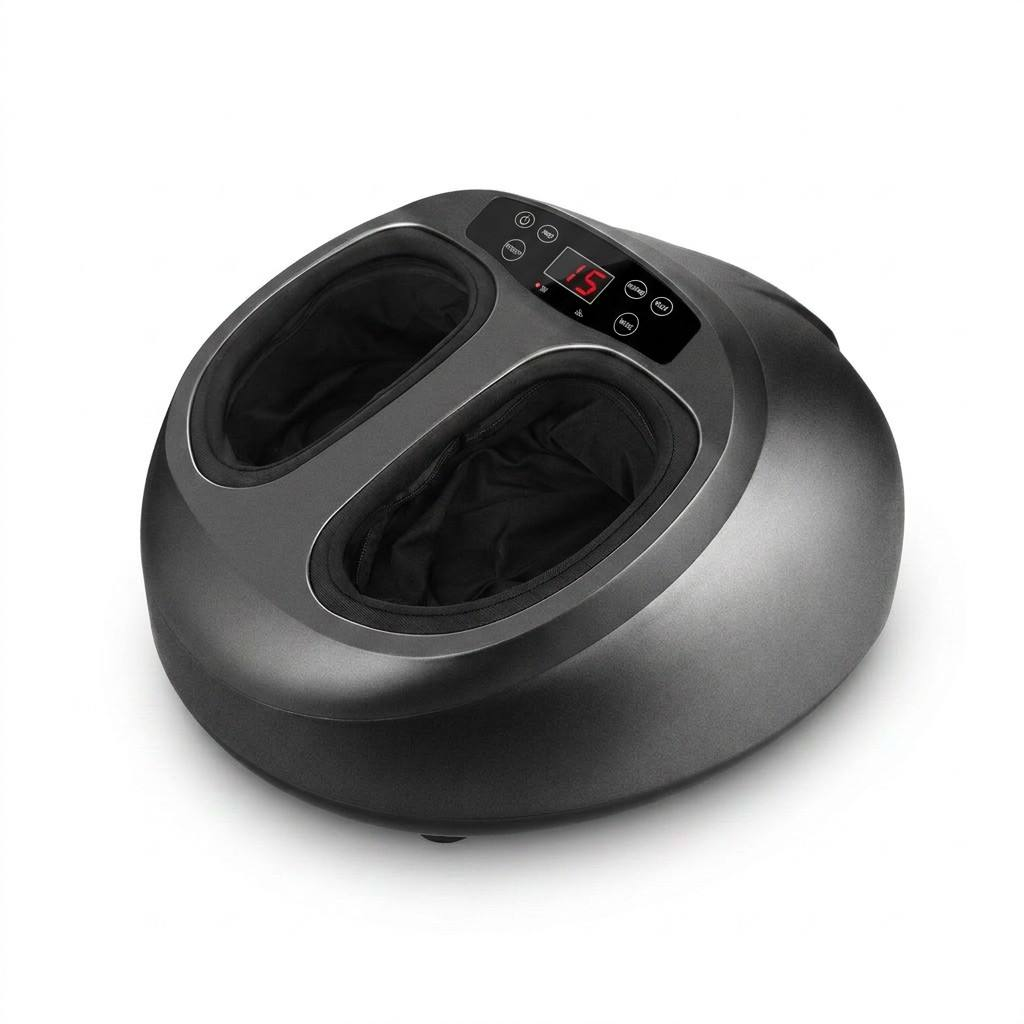
That request should never be met with hesitation. A factory willing to put you in a room with the actual mechanical or electrical engineers tends to catch design issues early, before they turn into costly tooling changes. Ask for a short call with the team after the first round of drawings, and pay attention to how clearly they explain material choices, motor placement, and heat dissipation.
You want a partner that already has a contingency plan, not one that treats that scenario as impossible. Look for evidence of buffer stock for common motors, rollers, and control boards, plus a clear change-order process with written cost and timeline impact before anything is modified. If the factory can show past examples of adapting without stalling shipment, that is a stronger sign than a promise.
This is one of the most overlooked questions until it becomes a dispute. The answer should be written into the agreement, not just stated verbally. Confirm whether the mold remains your property after the final order, whether CAD files and firmware are returned or destroyed, and what notice period applies if either side wants to exit. A factory that resists putting this on paper is usually not thinking long-term.
A final certificate is the bare minimum. Ask how many checkpoints exist during subassembly, whether they trace each batch back to specific component lots, and what their internal defect rate target actually is. Even better, ask if they allow third-party audits without weeks of advance notice. Factories with rigorous inline controls usually have no problem describing them in detail.
The best suppliers usually have a few concrete stories ready because they treat that as a normal part of their job. Listen for specifics: a wrong durometer on a kneading node, a subtle current spike in the power supply, or a cable strain issue found during lifecycle testing. Vague answers like 'we always check everything' tend to come from factories that rely on the customer to catch problems.
Long-term partnership means support continues after the last container leaves. Ask how many years they keep spare motors, control boards, remote controls, and molded shells, and whether they charge for storage or make spares available at a reasonable minimum order. If they struggle to answer, you may end up redesigning earlier than planned just because a simple component disappeared.
Every factory says they can handle peak season, but the mechanics matter more. Ask whether your orders get reserved production slots, whether they use a scheduling buffer, and how they communicate capacity constraints before accepting new work. A truthful answer may include limits, which is actually reassuring because it shows they will not overbook the line and quietly delay your shipment.
Conclusion
Before committing to a foot massager factory, most buyers focus on unit price and a decent pre-production sample, but that is exactly where long-term problems hide. You need to ask what actually happens when a shipment goes wrong—who absorbs the air freight, who reworks defective units, and how quickly replacement stock moves. A factory that cannot walk you through a real past failure is guessing. Quality also has to be proven beyond the first sample run; ask for data from repeat orders, inspection reports across multiple batches, and the names of clients who have been buying for more than a year. If the team that built your sample disappears after production starts, the consistency you paid for disappears with them, so confirm whether the same engineers and line leads stay on your project after year one.
Tooling changes are another test of how the manufacturer actually operates. When a mold needs adjustment, you want to know who makes the call, how much notice you get, and whether the cost is shared or dumped on you after the fact. Capacity and lead times matter just as much as the product itself. Some suppliers can handle a small trial order but struggle when your demand spikes in the fourth quarter, so press them on whether their production floor and labor pool can grow before your orders do. Peak season is where promises fall apart; ask for historical lead time data from September through December, not the off-season numbers they like to show. A long-term partner should be able to keep delivery dates when everyone else is overloaded.
Contact Us
Contact Person: Hannah
Email: [email protected]
Tel/WhatsApp: +86 18266954198
Website: https://www.okmassager.com/