Laser Safety Window Manufacturer: Essential Guide to Choosing Certified Optical Protection
2026-10-18
Finding a reliable laser safety window manufacturer is harder than it looks—certification claims are everywhere, but certified optical protection is not. Before you trust your eyes or your facility to a supplier, ask yourself: does the product actually meet the standards it claims? LASERPAIR has spent years cutting through industry hype, and this guide is built on that experience. Here’s what to look for when choosing certified laser safety windows.
Decoding Laser Classes and Matching Window Specs
Laser safety classifications aren't just labels; they dictate how much protection a viewing window actually needs. A Class 1 system is inherently safe, so a plain polycarbonate pane often does the job. But move up to Class 3B or Class 4, and suddenly you're dealing with beams that can damage eyes instantly, which means the window must block or attenuate the specific wavelengths in use.
Matching a window to a laser class starts with wavelength and optical density (OD). The window's data sheet will list an OD curve—typically above OD 6+ for Class 4 enclosures—but that number only matters at the wavelength it's rated for. A window rated for a 1064 nm Nd:YAG isn't automatically safe for a 532 nm frequency-doubled beam, so check the specs rather than assuming one pane covers all.
There's also the practical side: material, thickness, and how the window is mounted. Glass and acrylic each have different damage thresholds, and even a correctly rated window fails if the frame leaks light or if the pane is scratched. For higher classes, look for certified laser safety windows with full spectral data, and don't forget that viewing angle and beam exposure time can shift what's actually safe.
Certifications Worth Checking Before You Buy
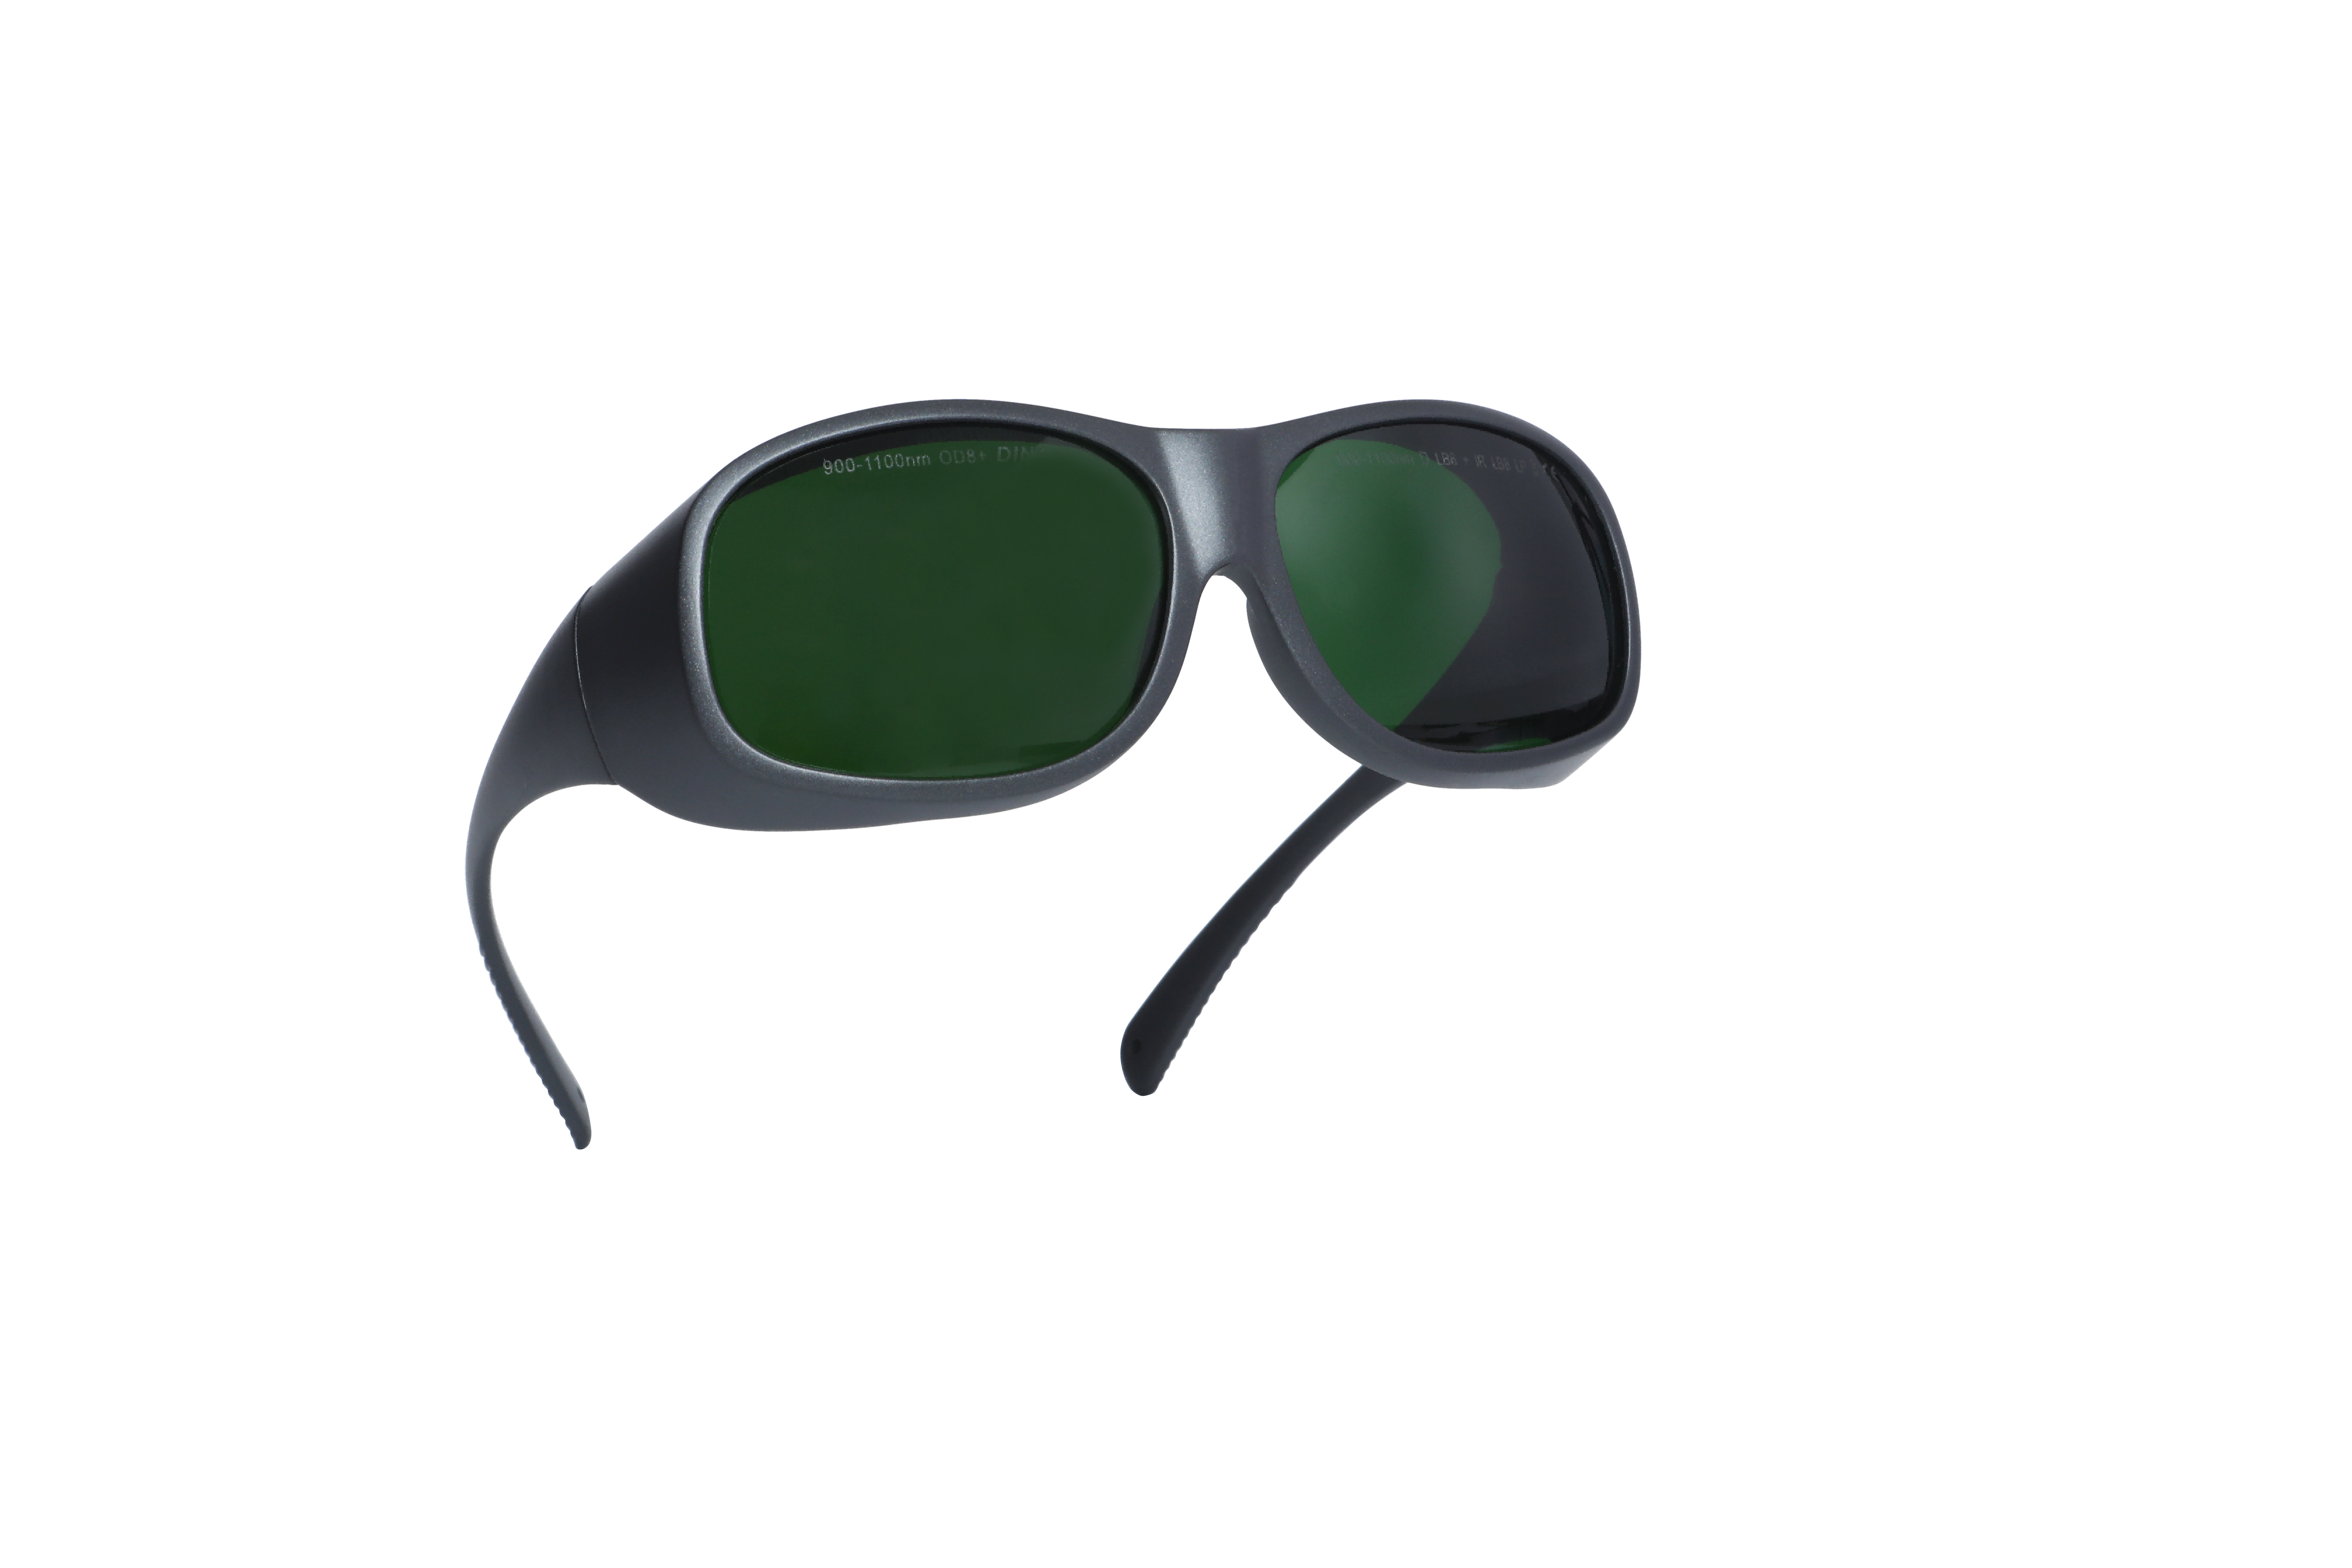
When you're comparing gadgets or appliances, the spec sheet rarely tells the whole story. Look for a UL or ETL mark before you buy anything that plugs into an outlet, since those indicate independent safety testing rather than just a manufacturer's claim. Energy Star is another one worth spotting on fridges, monitors, and power strips if you don't want your utility bill to creep up.
For clothing, bedding, or anything that touches your skin, OEKO-TEX Standard 100 is a useful shortcut. It means the fabric has been tested for a long list of harmful substances, which is more reassuring than words like gentle or natural on the tag. GOTS goes further for organic cotton and wool, covering the whole supply chain, while FSC is the one to look for on wooden furniture or paper products.
In the pantry and bathroom cabinet, certifications can cut through a lot of noise. USDA Organic has specific rules about synthetic pesticides and fertilizers, Fair Trade Certified focuses on labor conditions and fair wages, and Leaping Bunny indicates no new animal testing. A quick check of what each logo actually requires can save you from paying a premium for marketing fluff.
Material Trade-offs: Visibility, Durability, and Shielding
You rarely get a material that excels at all three. Glass, for instance, offers unmatched clarity but will shatter under impact and does nothing to stop electromagnetic interference. Metals do the opposite: they block signals and shrug off abuse, yet you cannot see through them. So the choice of material becomes a quiet negotiation, with each requirement pulling in a different direction.
Durability usually demands a trade with transparency. Polycarbonate and acrylic can take far more abuse than glass, but they scratch more easily and degrade under UV exposure. Adding a hard coat helps, but that coating can introduce a slight haze or reduce light transmission by a few percentage points. For a display window on a handheld device, that small loss might matter; for a static enclosure, it may not.
Shielding adds another layer of complexity. Conductive metals are excellent at blocking electromagnetic noise, but they are opaque. The workaround—embedding a fine wire mesh or using a transparent conductive film—either distorts the view or adds expense and fragility. A mesh fine enough to preserve clarity may still create moiré patterns, and a conductive oxide layer is easy to scratch. In the end, every material choice is a compromise, and the best solution often depends on which failure mode you can live with.
Custom Manufacturing for Unusual Mounts and High-Power Setups
When a standard bracket simply won't cut it, we step in. Our workshop has built custom mounts for everything from a vintage 10-inch refractor on a modern equatorial head to a side-by-side tandem rig carrying two 12-inch astrographs. Each piece starts as a conversation about balance, vibration, and the particular quirks of your optical tube assembly. We machine from billet aluminum or stainless steel, often adding tapped holes for accessories you haven't even thought of yet.
High-power setups bring their own headaches: mirror shift, flexure, and heat plumes from electronics. We've tackled these by designing low-profile dovetail clamps with oversized locking knobs, and by routing cable bundles through hollow sections so they don't act like sails in a breeze. One recent project involved a 16-inch Ritchey-Chrétien on a friction-drive mount—we fabricated a one-piece cradle that dropped total weight by 40% while doubling the stiffness.
The best part is that we don't just hand you a drawing and wish you luck. Every custom mount leaves our shop already stress-tested on a jig that simulates a full night of slewing and focusing. If something flexes or binds, we re-machine it before you ever bolt your telescope on. That's the difference between a piece of metal and a mount you'll trust at 400x on a windy ridge.
Testing Beyond the Data Sheet: What Manufacturers Should Prove
A datasheet can list impressive bandwidth, low noise, and power figures, but those numbers are often captured under ideal lab conditions that rarely survive contact with real installations. Manufacturers need to demonstrate how their components behave when thermal loads cycle unevenly, when supply rails sag beneath nominal values, or when adjacent channels inject interference. Customers deserve evidence that a part will hold its specified performance after repetitive stress, not just during a five-minute bench evaluation.
Long-term drift is another area where glossy specifications fall silent. A precision reference or analog front-end may look superb on day one, yet degrade quietly as moisture, bias currents, and package stresses take their toll. Responsible manufacturers should publish accelerated life test data, showing offset shifts after thousands of hours at elevated temperature and humidity. This kind of proof builds far more confidence than a single line of typical values, because it tells engineers how much margin they must budget for years of field service.
Finally, true differentiation comes from proving behavior under failure and abuse scenarios that no datasheet parameter captures. What happens to the output stage when a load shorts abruptly? Does the device recover gracefully from an electrostatic discharge event, or does it enter a latch-up state that requires a power cycle? By sharing test reports on reverse polarity, overvoltage transients, and sustained output clamping, manufacturers show they understand the messy realities outside the test bench. That evidence separates commodity silicon from components worth trusting in safety-critical designs.
Installation and Maintenance Habits That Keep Protection Intact
Getting the film or coating to stay put starts well before the first squeegee pass. Any residue from polish, wax, or even fingerprint oils will weaken the bond at the edges, which is exactly where failures begin. Wipe the surface with a diluted alcohol solution using a clean, lint-free cloth, then let it flash off completely. Work in a space without moving air if possible; tiny dust particles trapped under the material create micro-lift points that turn into peeling later. When laying the film, keep tension even rather than stretching hard around bends. Overstretched adhesive loses its ability to recover, so curved areas become the weak link. Leave a consistent margin of a millimetre or two at the border so routine wiping doesn't catch the edge and start a peel.
Right after installation, give the adhesive time to cure before introducing water or pressure. A few days of dry weather is ideal, but if you must drive in rain, avoid high-pressure washes and automatic brushes for at least a week. When you do wash, use a pH-neutral shampoo and a soft mitt, working from the top down so grit doesn't get pushed against the seams. Rinse thoroughly with a gentle stream, not a jet aimed at the edges. Drying matters more than people think: pat the surface with a plush microfiber towel instead of dragging it across the film. A dragging motion can catch a slightly raised edge and tear it, opening a path for dirt and moisture.
Even a perfectly installed layer needs periodic attention to stay intact over the long haul. Once a month, run your fingers along the edges and around any cutouts to feel for lifting. If you catch a small peel early, a brief application of low heat and a soft roller can press it back before contamination gets underneath. Left alone, a lifted edge will collect wax, road grime, and moisture, slowly spreading the failure. Reapplying a light sealant every few months helps the surface shed water and UV instead of absorbing it. Try to avoid parking under trees that drop sap or in spots where sprinklers blast mineral-heavy water at one panel all morning; these slow, repetitive exposures do more damage than a single heavy storm.
FAQ
A certified window is tested and labeled for specific wavelengths and optical density levels, while tinted acrylic may only reduce visible light and offer no proven protection. Look for independent test reports, EN 207 or EN 208 ratings, and permanent markings that show the exact protection range.
At minimum they should provide documentation for EN 207 or EN 208 for European compliance, or ANSI Z136.1 and optical density ratings for U.S. applications. Some also follow IEC 60825. Ask for traceable test certificates from an accredited lab rather than relying on a CE mark alone.
Match the optical density to your laser's wavelength and maximum output power. For example, a Class 4 1064 nm laser often requires OD 5+ at that specific wavelength, but the same window may stay transparent to an alignment beam. Base the calculation on accessible emission limits and intended exposure duration.
Acrylic and polycarbonate are lightweight and work well for larger panels, while glass offers better scratch resistance and chemical durability. Coatings matter more than the base material: multi-layer coatings achieve high OD at narrow wavelength bands, while absorptive dyes cover broader bands but may degrade over time.
Yes, many manufacturers offer custom cutting, edge finishing, and even curved or angled panels. Provide precise dimensions, mounting method, and the laser parameters. Also confirm that the certification remains valid after custom fabrication, since cutting outside the optical aperture usually does not change the protective properties.
Ask for the test report showing optical density versus wavelength, the standard it complies with, whether the marking is permanent, the expected lifetime under your laser's power density, and whether they can guarantee batch-to-batch consistency. Also ask about warranty and replacement criteria if any spotting or bleaching appears.
Inspect monthly for pitting, crazing, delamination, or coating damage. Replacement timing depends on power density and exposure, but any visible damage within the beam path means the window should be taken out of service immediately. Keep a log with installation date and test reports for audit.
Choosing by price or color alone, ignoring the wavelength match, assuming a standard polycarbonate sheet is safe, or forgetting that visible light transmission does not equal laser protection. Another mistake is relying on a supplier's verbal guarantee without independently verifying the certification.
Conclusion
Selecting a laser safety window starts with matching the window's optical density and wavelength coverage to the exact laser class in your facility—a Class 4 system demands far more robust attenuation than a Class 1 enclosure. Check for certifications like CE and EN 60825, and ask for the full test report rather than a simple declaration. Material choice is not just about shielding: polycarbonate offers impact resistance but scratches easily, while acrylic provides better visible light transmission yet can degrade under UV. A reputable manufacturer will be upfront about these trade-offs and help you balance visibility, durability, and attenuation for your specific beam parameters.
For unusual mounts or high-power setups, custom manufacturing should include edge finishing, frame integration, and thermal management—not just a cut sheet. Demand that manufacturers prove performance beyond the data sheet with third-party testing for optical density at your exact wavelengths, damage threshold, and long-term stability under continuous exposure. Once installed, protection only holds if you follow correct handling and maintenance: inspect for pitting or crazing, clean with approved solvents, and re-verify alignment after any service. A certified window is a system, not a component, and the right manufacturer will treat it that way.
Contact Us
Contact Person: Jenny
Email: [email protected]
Tel/WhatsApp: +86 13537713281
Website: https://www.laserpair-safety.com/