Motorcycle Parts Vertical Lift Plating Equipment: What to Know Before Buying
2026-11-02
Electroplating motorcycle parts isn't just about shine—it's about corrosion resistance, wear protection, and that flawless finish riders expect. Yet choosing the right vertical lift plating equipment can make or break your production line. Before you invest, there are critical factors most buyers overlook, from tank geometry to automation control. At Junda, we've seen how the wrong setup leads to uneven coating and costly rework. This guide cuts through the noise and gives you the practical checklist you need to buy with confidence.
Load Ratings That Match Your Heaviest Part
Most people pick a shelf, caster set, or cart based on a rough guess—then wonder why it sags, wobbles, or stops rolling. Instead of guessing, find the single heaviest item you'll ever place on the unit and use that as your baseline. Weigh the object or check its spec sheet, then add a small buffer for tools, spills, or that one extra box someone always drops on top.
A load rating that matches your heaviest part doesn't just prevent failure; it also keeps you from paying for capacity you'll never use. If your heaviest drawer holds 70 pounds of hardware, a 100-pound rating gives you breathing room without the extra weight and cost of a 300-pound industrial unit. Matching the rating to the real peak load keeps the equipment nimble and affordable.
Keep in mind that most printed ratings assume evenly distributed weight. If your heaviest part will sit on one corner, or the unit gets moved while loaded, step up to the next rating tier. That small jump accounts for the uneven stress that static numbers don't show, so the wheels still turn and the frame stays square after years of daily use.
Why Vertical Travel Affects Coating Thickness
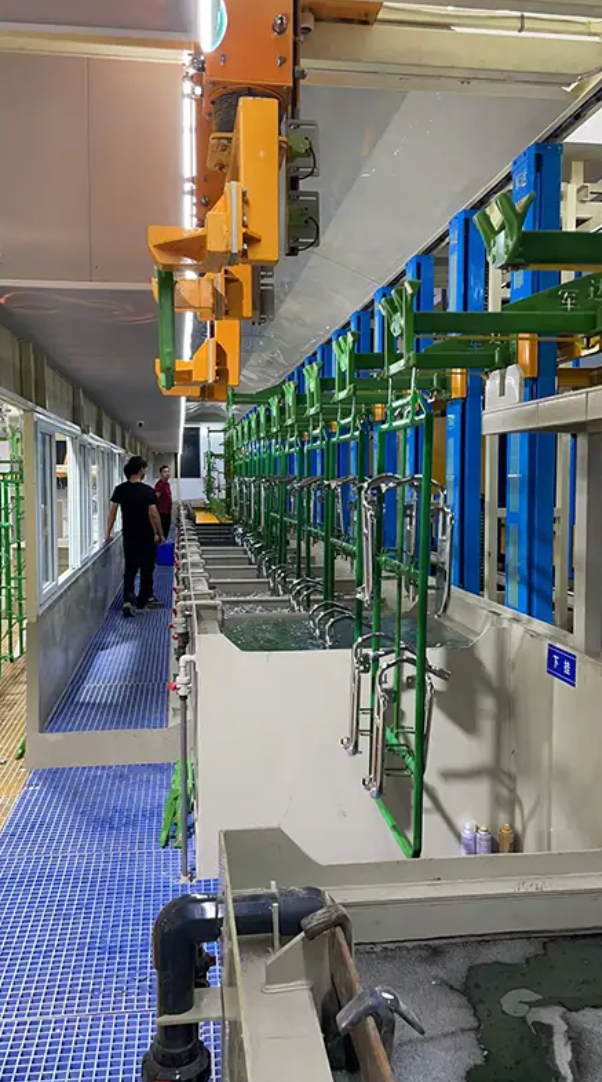
When a part moves vertically through a coating bath, the speed at which it exits the liquid directly shapes the wet film left behind. A faster pull rate drags more fluid upward before gravity can pull it back, so the coating lands thicker. Slow the travel down, and gravity wins more decisively—excess liquid runs off, leaving a thinner, more uniform layer. This simple balance between upward motion and downward drainage is the core reason vertical travel changes final thickness.
The effect isn't limited to dip tanks. In spray applications, vertical stroke speed alters how long the spray pattern dwells on any given band of surface. Slow vertical travel lets more material accumulate in one pass; quick travel spreads the same output over a taller area, reducing local build. Edge geometry and part temperature further complicate the picture, but the travel rate remains the primary dial for adjusting thickness without reformulating the coating.
Operators often notice that the top of a vertically coated part ends up slightly thinner than the bottom after curing, even when the initial application looks even. That gradient traces back to gravity-driven flow during the first seconds after contact. Coating at the lower end receives runoff from above, while the upper region loses material as it drains. Controlling vertical travel speed and dwell time between stations is therefore a practical way to keep thickness within tolerance across the full height.
The Grease Points and Seals You'll Be Replacing
When you start pulling the old components apart, the first thing you'll notice is how much of the original grease has turned into a thick, gritty paste. It stops lubricating and starts acting like sandpaper on every pivot and bushing. Cleaning out those cavities takes time, but skipping it just means the new parts will wear out twice as fast. Pay close attention to the steering knuckles and the ball joints—those are where the old grease tends to bake on hardest.
As for the seals, don't assume they're reusable just because they look intact. The rubber gets hard and loses its flex over the years, so even a tiny crack will let water and road grit in. Pull them out carefully with a pick, but avoid scoring the metal seats. If the seal lip has any flat spots or you can feel a groove with your fingernail, replace it without a second thought. A fresh seal costs a few dollars; a ruined bearing or joint costs a lot more in downtime.
Before you press anything back together, pack the new grease by hand rather than relying on a gun. Work it into the rollers or between the balls until you see it squeezing out the sides—that's how you know there are no dry pockets. Then wipe the sealing surfaces completely clean with a lint-free cloth. Any leftover grit from the old assembly will chew through the new seals within the first hundred miles. Take your time here, and the whole job will feel tighter and quieter than the day the truck rolled off the line.
Clearance Requirements Nobody Mentions in Brochures
When a spec sheet lists a 30-inch range, it’s rarely telling you that the real number you need is closer to 36 once the oven door swings open and the rear vent gets hot. Brochures love to show sleek installations with zero side gaps, but the fine print (if it exists) usually ignores the fact that adjacent cabinetry needs an extra two to three inches of thermal breathing room—or your quartz countertop starts to discolor within a year.
Also watch for vertical clearance nobody prints: a built-in microwave over a range might clear the cooktop by 13 inches, but if you actually cook with tall stockpots or a pressure canner, you’ll be tilting them at an angle and spilling every time. Delivery crews won’t mention that your 1920s doorway is three inches too narrow until the unit is on the dolly and the box is torn open.
Before you trust the cutout template, measure the actual swing radius of every handle and hinge, and add a half-inch for floor unevenness. That’s the clearance requirement that saves your back, your walls, and your marriage.
Interlocks and Guards Worth Paying Extra For
When a machine guard trips mid-cycle, the difference between a standard interlock and a pricier reinforced model shows up fast. Cheap switches tend to wear at pivot points and can be bypassed with a zip tie in seconds. Paying extra for a tongue-actuated interlock with a locking solenoid, on the other hand, keeps the panel from opening until motion has fully stopped. That single upgrade has saved more than one operator from a crushed hand and kept a production line from an unplanned shutdown.
Guards are not just metal cages anymore. Some worth the higher price tag include polycarbonate viewing panels with anti-fog coatings and frames that absorb impact without cracking. Others have captive fasteners so panels can't be left off after cleaning. Interlocks with RFID-coded actuators cost more but they stop the old trick of taping a spare key into the switch. Those small design choices add up to a work area where safety doesn't depend on everyone following the rules perfectly.
Maintenance teams often note that premium interlocks and guards end up costing less over three or four years. A robust hinge, a sealed switch housing, and a guard that doesn't rattle loose cut down on nuisance trips and replacement parts. Budget versions fail gradually, and each failure invites a temporary bypass that becomes permanent. Spending extra up front on the right guard and interlock combo is usually cheaper than one incident report, one OSHA fine, or one week of downtime.
Utility Costs That Show Up After Installation
Most people budget for the upfront price of a new system or appliance, but few anticipate the quieter drain that begins the moment it's switched on. A new water softener, for instance, might quietly add a few extra regeneration cycles each week, each one pulling gallons of water and a burst of electricity. Those incremental costs don't announce themselves—they simply appear on the next utility statement, often buried among seasonal fluctuations.
The real surprise usually arrives with the first full billing cycle after installation. An outdoor kitchen with a dedicated refrigerator and ice maker can push a monthly electric bill up by twenty or thirty dollars, while a tankless water heater might spike gas usage in ways the sales brochure never mentioned. These aren't defects; they're simply the ongoing operational costs that only become visible once the equipment is actually running day after day. Homeowners who track their usage closely can spot the pattern, but many simply absorb the higher bills without connecting them to the recent upgrade.
FAQ
Look beyond the tank size. The lifting stroke and racking design determine how evenly small, oddly shaped parts like brackets or levers get coated. A machine with adjustable speed and dwell time in each station gives you much better control over thickness on threaded areas and recesses.
It's often overlooked. You need a rectifier that can deliver stable low-ripple DC, especially for chrome or nickel on cast aluminum or steel motorcycle components. If the ripple is too high, you'll get dull or burnt deposits. Match rectifier capacity to your largest load, not your average one.
Yes. Polypropylene tanks handle most acid zinc and nickel baths well, but if you're running chrome, make sure the tank lining and heating elements can resist chromic acid. Ask about the tank wall thickness and welded corners—cheap thin walls warp over time and leak at seams.
Underestimating the ventilation and waste treatment side. Plating mist and rinse water from motorcycle parts contain heavy metals and acids. You'll need a scrubber or mist eliminator and a way to neutralize and treat wastewater. Skipping this leads to compliance trouble and unsafe working conditions.
Motorcycle parts include everything from flat washers to deep-dish covers. Deep recesses and blind holes need good solution agitation—look for air sparging or eductor circulation built into the tanks. Without it, you'll get thin plating inside recesses no matter how long you leave the rack in the bath.
For a small shop doing batches of mixed parts, a manual or semi-auto hoist with programmable recipes per rack is usually more flexible than a fully automatic line. You can change dwell time or current on the fly when you see a problem. Fully automatic pays off only when you run the same part families day after day.
Continuous filtration keeps particulates from rough plating. Use a filter rated for the bath temperature and chemical type. Schedule anode cleaning and bus bar tightening monthly, because loose connections cause uneven current distribution and overheating. Also check the lift cables or chains for stretch—misaligned racks dip unevenly.
It can be, but only if you inspect the frame for corrosion, verify the rectifier output with a load bank, and check the hoist limit switches. Replacing a damaged tank or rewiring a control panel often eats up the savings. Get maintenance records if possible, and budget for re-lining tanks that handled aggressive chemistries.
Conclusion
Before you commit to a vertical lift plating line for motorcycle parts, pull the heaviest bracket, fork tube, or brake caliper off your bench and check its true wet weight—not the dry spec. If the lift's rated capacity is based on a balanced load and your racks hang unevenly, you'll be rebuilding the carriage sooner than expected. Vertical travel distance is just as critical as tank depth: too fast a withdrawal and the coating thins at the bottom of a fork leg; too slow and you burn time on every cycle. Ask the builder for a dwell-and-withdraw curve, not just a speed dial.
The less glamorous costs show up after the first month. Grease zerks on the lift column, wiper seals around the tank lip, and the lower guide bearings all wear against plating solution mist, so budget for replacements and make them easy to reach without draining the line. Check actual ceiling clearance with the carriage at full stroke; many brochures omit the extra 10–14 inches needed for a slung rack to clear the anode bar. Interlocks that stop travel if a guard is open and a physical shield over the chain or screw drive are worth paying for—crushed fingers are not a warranty item. And compare utility draw: rectifier efficiency, tank heating, and exhaust fan run time can add several hundred dollars a month to a line that looked cheap at quote.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com