Top 10 Air Cooled Hydraulic Piston Pumps for Ceramic Filter Presses
2026-08-17
Choosing the right hydraulic piston pump for a ceramic filter press can make or break your operation—overheating, pressure drops, and costly downtime are just the beginning. That’s why we’ve dug into the market to bring you a practical rundown of the top 10 air-cooled models that actually hold up in demanding filtration cycles. Whether you’re upgrading an aging system or speccing a new line, this list cuts through the noise. And if you’re already leaning toward proven reliability, Sinou offers a lineup worth a closer look before you commit. Here’s what you need to know.
The Real Reason Ceramic Filter Presses Punish Ordinary Hydraulic Pumps
Ceramic filter presses demand constant, unyielding pressure to squeeze every last drop of moisture from dense slurry. Ordinary hydraulic pumps simply aren't built for that kind of marathon. They spike, they fade, they cavitate under the sustained load, forcing the system to compensate with extra cycles and wasted heat. The result is a pump that works twice as hard for half the output, wearing seals and valves at an alarming rate.
The real punishment comes from the pressure profile itself. Ceramic slurries are abrasive and inconsistent, causing micro-fluctuations that ordinary pumps interpret as demand surges. Each surge slams the internal components, creating stress fractures in the piston shoes and scoring the cylinder walls. Before long, the pump loses its ability to hold a steady pressure plateau, and the filter press starts producing cakes with uneven moisture content — a silent killer for ceramic quality.
What makes it worse is that many operators blame the filter press, not the pump. They adjust cycle times, tweak the cloth tension, or add flocculants, when the real culprit is a hydraulic heart that's slowly tearing itself apart. A pump designed for general industrial use can't survive the relentless, abrasive, high-pressure grind that ceramic filtration demands day after day.
Why Air-Cooled Piston Units Outlast Water-Cooled Rivals in Clay Dust Environments
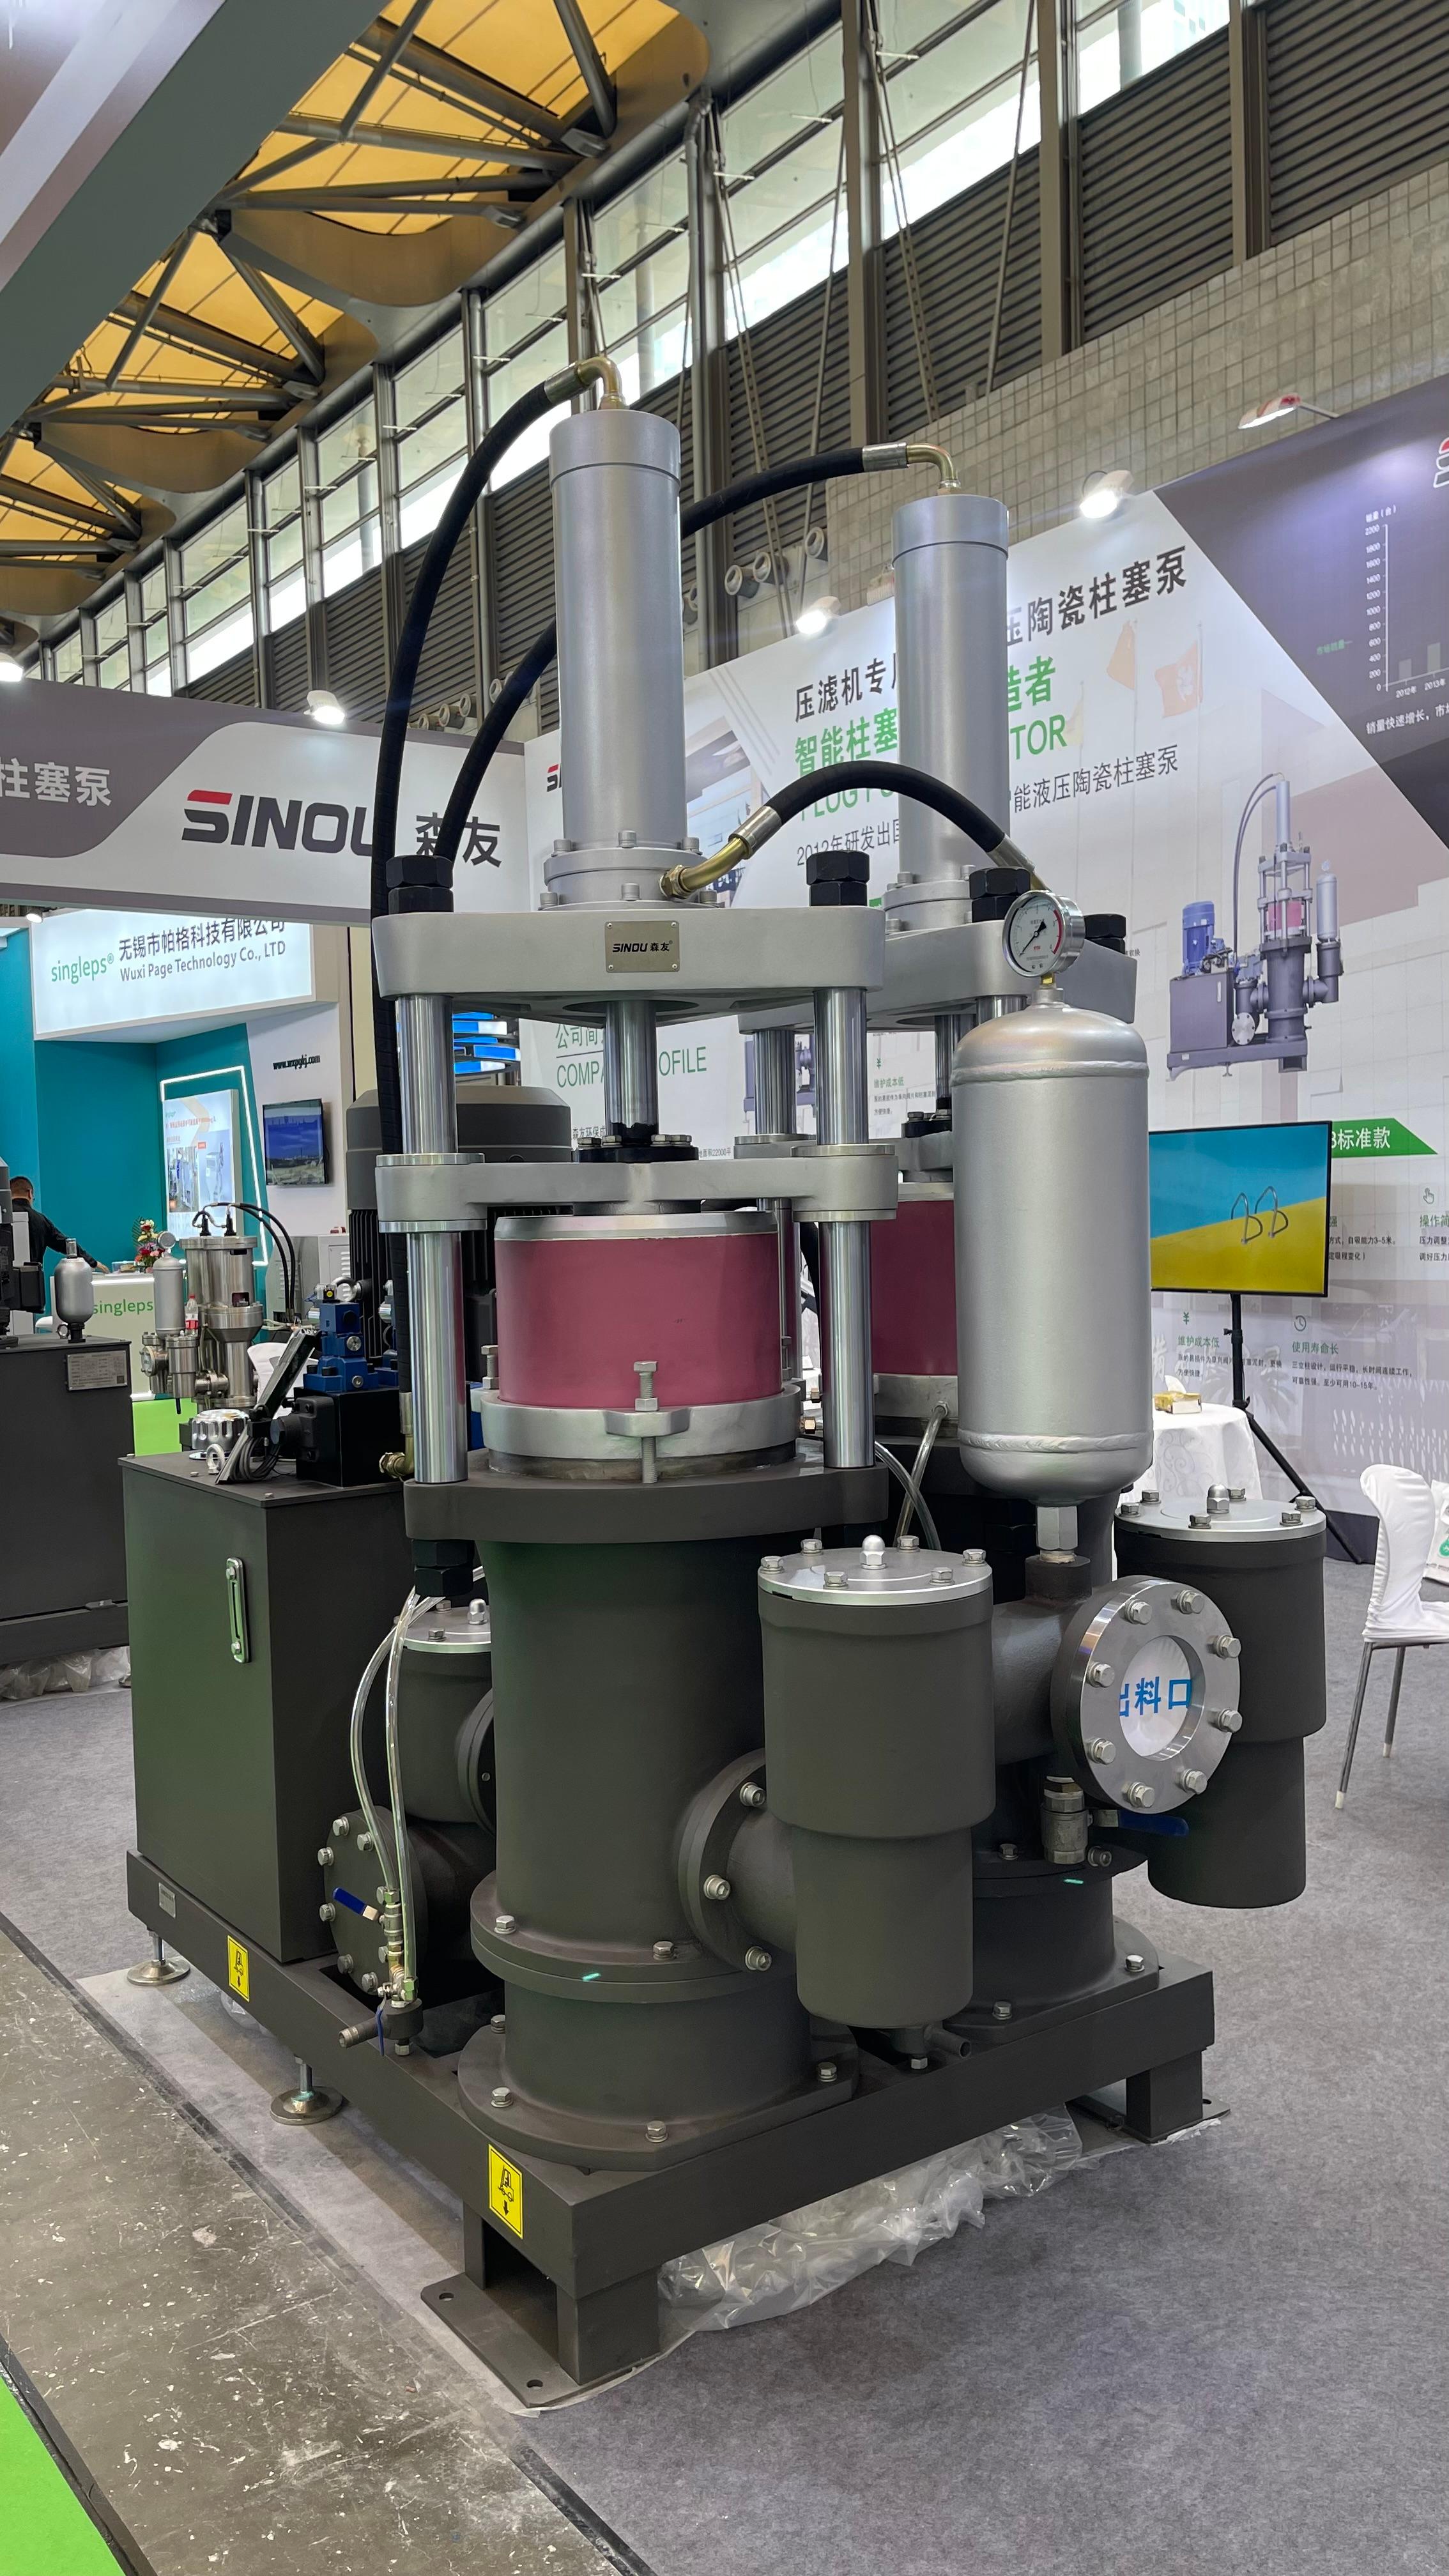
Water-cooled systems look tough on paper, but clay dust finds every weak seam. Radiators and coolant passages clog within weeks when fine silica particles mix with moisture, turning into a gritty paste that blocks heat exchange. Air-cooled piston units skip that entire failure chain. No radiator fins to pack with mud, no coolant to turn abrasive, no water pump seals to eat themselves alive. The cooling fins on an air-cooled cylinder are wide open and self-clearing under normal vibration, so dust sheds before it can build a thermal blanket.
Clay environments punish any machine that relies on liquid moving through narrow paths. Every hose clamp, gasket, and drain plug becomes a potential mud injection point. Once that slurry gets inside a water jacket, it settles in low spots, bakes onto hot surfaces, and silently reduces cooling capacity until the engine cooks itself. Air-cooled designs don't have those hidden pockets. Heat leaves directly through finned metal to the surrounding air, and if dust accumulates, a quick blast with compressed air restores full performance. No draining, no flushing, no corrosion inhibitor top-ups.
Longevity in clay dust isn't just about surviving one bad week—it's about tolerating thousands of hours of fine abrasive particles working into every crevice. Water-cooled rivals demand constant filter changes, coolant analysis, and pressure checks. Their downtime stacks up fast when clay turns service intervals into daily chores. Air-cooled piston units run leaner on maintenance because the cooling system has no liquid to contaminate, no pressure to leak, and far fewer parts that can clog. That's why operators in brickworks, ceramic plants, and dry clay mines keep choosing them decade after decade, even when water-cooled specs look competitive on a brochure.
Pressure Profile of a Filtration Cycle: Where Pump Failures Actually Start
Most operators assume pump failures trace back to worn seals or cavitation, but the real story hides earlier in the cycle. The pressure profile of a filtration run is rarely flat. It climbs as solids accumulate on the media, then shifts sharply when backwash or purge begins. That transition zone, where pressure drops from peak to near zero within seconds, exerts a force few pumps are designed to handle repeatedly.
At the start of each cycle, the pump works against low resistance. Flow is high, pressure modest. As the cake builds, the pump's operating point moves left on its curve, often toward shutoff head. If no bypass or variable speed control exists, the pump can deadhead momentarily before the cleaning phase kicks in. Then the sudden release sends a pressure wave backward through the discharge piping, hammering check valves and flexing impeller vanes. Over months, microcracks form at the vane roots, not at the seal.
The failure signature is misleading. Maintenance logs show seal replacements and bearing wear, but the initial damage occurs during that repeated spike-and-crash of pressure. To extend pump life, operators should map a full cycle with a high-speed transducer, not just a panel gauge. The data typically reveals a pressure overshoot of 20-40% above steady-state during the first seconds of backwash. Dampening that transient, with a surge tank or softer valve actuation, is where real reliability begins.
Matching Displacement to Cylinder Speed Without Oversizing the Motor
Hydraulic systems often suffer from a basic mismatch: the cylinder moves either too slowly for the cycle time or demands a motor so large that energy bleeds away as heat. The key is to work backward from the cylinder's required velocity. Calculate the flow rate needed to extend or retract the piston at the target speed—this is simply piston area times velocity. With that flow rate known, choose a motor displacement that delivers it at a sensible operating speed, typically near the motor's efficient range rather than at a crawl or a scream.
Oversizing the motor creeps in when engineers add a safety factor to the displacement "just in case." That extra displacement pushes the motor into a low-speed, high-torque corner where volumetric efficiency drops and internal leakage rises. You end up paying for a bigger frame, more oil cooling, and a pump that never gets to run in its sweet spot. A better approach is to match displacement closely to the calculated flow demand, then let the pressure compensator or variable-speed drive handle minor fluctuations. This keeps the motor lean enough to respond quickly without sacrificing the force needed at the cylinder.
One practical trick is to compare the motor's displacement per revolution against the cylinder's volume per stroke. If the cylinder needs, say, three liters to complete its stroke in two seconds, the motor must supply 90 liters per minute. A motor with 45 cc/rev would need to spin at 2000 rpm—reasonable for a small unit. But choose 100 cc/rev and that speed drops to 900 rpm, often below the motor's best efficiency band. So the motor grows in size, the system grows in cost, and nothing gets faster. Matching displacement without oversizing is not about minimizing motor size; it's about letting the cylinder's speed dictate the motor's rhythm.
Heat, Noise, and Leakage: Three Field Measurements That Separate the Best Ten
Lab results can make almost any product look decent, but real-world field tests separate the genuinely strong performers from the rest. Heat, noise, and leakage are the three measurements that consistently expose those differences. Heat tells you whether a unit actually holds its set temperature without cycling excessively or wasting energy. Noise reveals how much constant hum or abrupt rattling you’ll live with day after day. Leakage is the most overlooked factor: even a small gap lets conditioned air slip out and outside air creep in, undermining both comfort and efficiency.
When you rank the best ten, you’re not just looking for one standout metric—you’re looking for balance. A product with excellent heat control but poor leakage will still leave you with cold drafts and inflated bills. A whisper-quiet model that can’t maintain temperature under load isn’t much better. The top performers tend to hold all three measurements within a narrow range, and field tests catch the subtle failures that controlled chambers miss. That’s why heat, noise, and leakage together make a sharper cutoff than any single specification.
Service Intervals, Seal Kits, and What Maintenance Logs Rarely Show
Factory service intervals read like a promise: change this at 500 hours, rebuild that at 2,000. But any field tech who has pulled a cylinder apart knows the hour meter only tells part of the story. Dust, moisture, pressure spikes, and even the way a machine idles through winter can chew through seals long before the manual says to care. A seal kit ordered at the prescribed interval often arrives after the damage is already done, leaving you with scored rods and contaminated oil that no scheduled maintenance plan accounted for.
Seal kits themselves are not all equal. The generic polyurethane lip seal might hold fine on a clean indoor press, yet fail early on a coastal excavator working in salt spray and fine silt. What maintenance logs rarely show is the small weep that starts at hour 800, only to become a full bypass by hour 820. By the time the fluid stain appears on the shop floor, the log still says everything is on schedule. That gap between recorded service and real-world wear is where downtime breeds.
A better approach treats the interval as a starting point, not a law. Pull a sample of hydraulic oil, check for rising particulate counts, and look for the faint varnish or dampness at the rod wiper. If a seal kit is going in, inspect the groove, the backup rings, and the rod surface for micro-scoring that the naked eye misses at first glance. Logs rarely show the operator who runs the boom against the relief valve every afternoon, but the seals remember. Maintenance that respects that memory will always beat a calendar.
FAQ
Air cooled pumps eliminate the need for a constant cooling water supply, which is a major advantage in ceramic plants where water quality often leads to scaling or corrosion inside heat exchangers. They also reduce auxiliary piping and maintenance associated with water circuits. In hot, dusty environments, a well-designed air cooled unit with a large finned cooler can match thermal stability without the risk of water leaks contaminating the hydraulic oil.
Start by calculating the total oil volume required to close the press, fill the diaphragm, and hold pressure during the cake formation phase. Then factor in the cycle time target and the maximum working pressure the filter plates can tolerate. A common mistake is choosing displacement based only on motor horsepower; instead, look at delivered flow at the highest pressure point, not at low load. For most ceramic filter presses, a pump that provides 80 to 120 liters per minute at peak pressure with a 15 to 20 percent reserve works well.
The biggest factors are piston surface treatment, seal material, and the cleanliness of the hydraulic oil. Ceramic plants are notoriously dusty, so pumps with hardened or coated pistons resist abrasive wear from fine particles that enter through breathers. Seal compatibility with high temperatures and the occasional oil contamination is equally important. Also, a built-in relief valve with a dampened response prevents shock loads when the filter press reaches full clamping force.
Yes. The cooling fins need frequent cleaning because clay dust and slurry mist settle on them and drastically reduce heat dissipation. Unlike water cooled units, there is no water filter or scale inhibitor to check, but you should monitor oil temperature closely during long pressing cycles. Changing hydraulic oil on schedule and checking the breather element every two to three months are more critical here than in general industrial applications.
Pressure spikes usually come from fast closing valves or rigid piping rather than the pump itself. When the filter press reaches the end of its travel, kinetic energy in the oil column creates a sharp rise before the relief valve can react. Using a pump with a pilot operated relief valve and adding a small accumulator or flexible hose near the cylinder can absorb these spikes. Also check that the directional control valve is not shifting too abruptly during decompression.
A single hydraulic power unit can run several presses if they do not demand peak flow at exactly the same time. The trade-off is that pressure and speed become interdependent; when one press is closing, another might starve for flow, leading to longer cycle times. For two or three smaller presses, a common pump with priority flow control can work, but for anything larger, separate pumps or a variable displacement pump with load sensing gives much smoother operation and avoids frequent unloading.
Pump alignment, inlet pipe diameter, and ventilation around the cooler are frequently ignored. A slightly misaligned coupling can destroy shaft seals within weeks, and an undersized suction line causes cavitation that sounds like a rod knock. Air cooled pumps need at least 30 centimeters of clear space around the fan intake and exhaust; otherwise, hot air recirculates and the oil temperature climbs during long filter cycles. Mounting the pump on vibration isolators also reduces noise transmitted through the steel platform.
Most air cooled piston pumps produce between 75 and 88 decibels at one meter, but the perceived noise depends heavily on the fan design and the pump's operating speed. Some brands use large, slow turning fans that move more air with less high frequency whine, while others use smaller high speed fans that are more intrusive. The piston pump itself contributes a rhythmic mechanical noise that varies with pressure. If noise is a concern, look for a pump with a cast iron housing and an integral rubber mounting base, and avoid running the pump at maximum displacement for extended periods.
Conclusion
Ceramic filter presses don’t just wear out hydraulic pumps; they attack them in ways that only become obvious after the first unplanned shutdown. The filtration cycle is not a steady load, and the pressure profile ramps sharply at the end of each cycle, hammering piston seals and valve plates. In a clay dust environment, water-cooled units clog and overheat long before their rated life, while air-cooled piston pumps keep their cooling surfaces clear and tolerate the dust that finds its way into every crevice. Matching displacement to the clamp cylinder speed matters more than raw horsepower, because an oversized motor simply pumps more heat into the oil and shortens seal life. The best ten models on this list all handle the initial squeeze, the holding phase, and the return stroke without pushing the system beyond its thermal ceiling.
Field measurements separate the contenders from the pretenders. Heat, noise, and leakage are not abstract specs; they are what a maintenance tech sees with an infrared gun, a decibel meter, and a drip pan. When two pumps share the same displacement, the one that runs 15 degrees cooler and 4 decibels quieter is usually the one that will still be holding pressure at the next scheduled filter cycle. Service intervals tell a similar story. Seal kits and bearing replacements are unavoidable, but the logs rarely show how often a pump was nursed through a shift with a partial bypass or a topped-up reservoir. The top ten listed here earned their places by staying boring in the field, with fewer leaks, less noise, and longer stretches between seal kit changes than their water-cooled rivals.
Contact Us
Contact Person: HaiYan
Email: [email protected]
Tel/WhatsApp: +86 18957325588
Website: https://www.senyoubeton.com/